EN


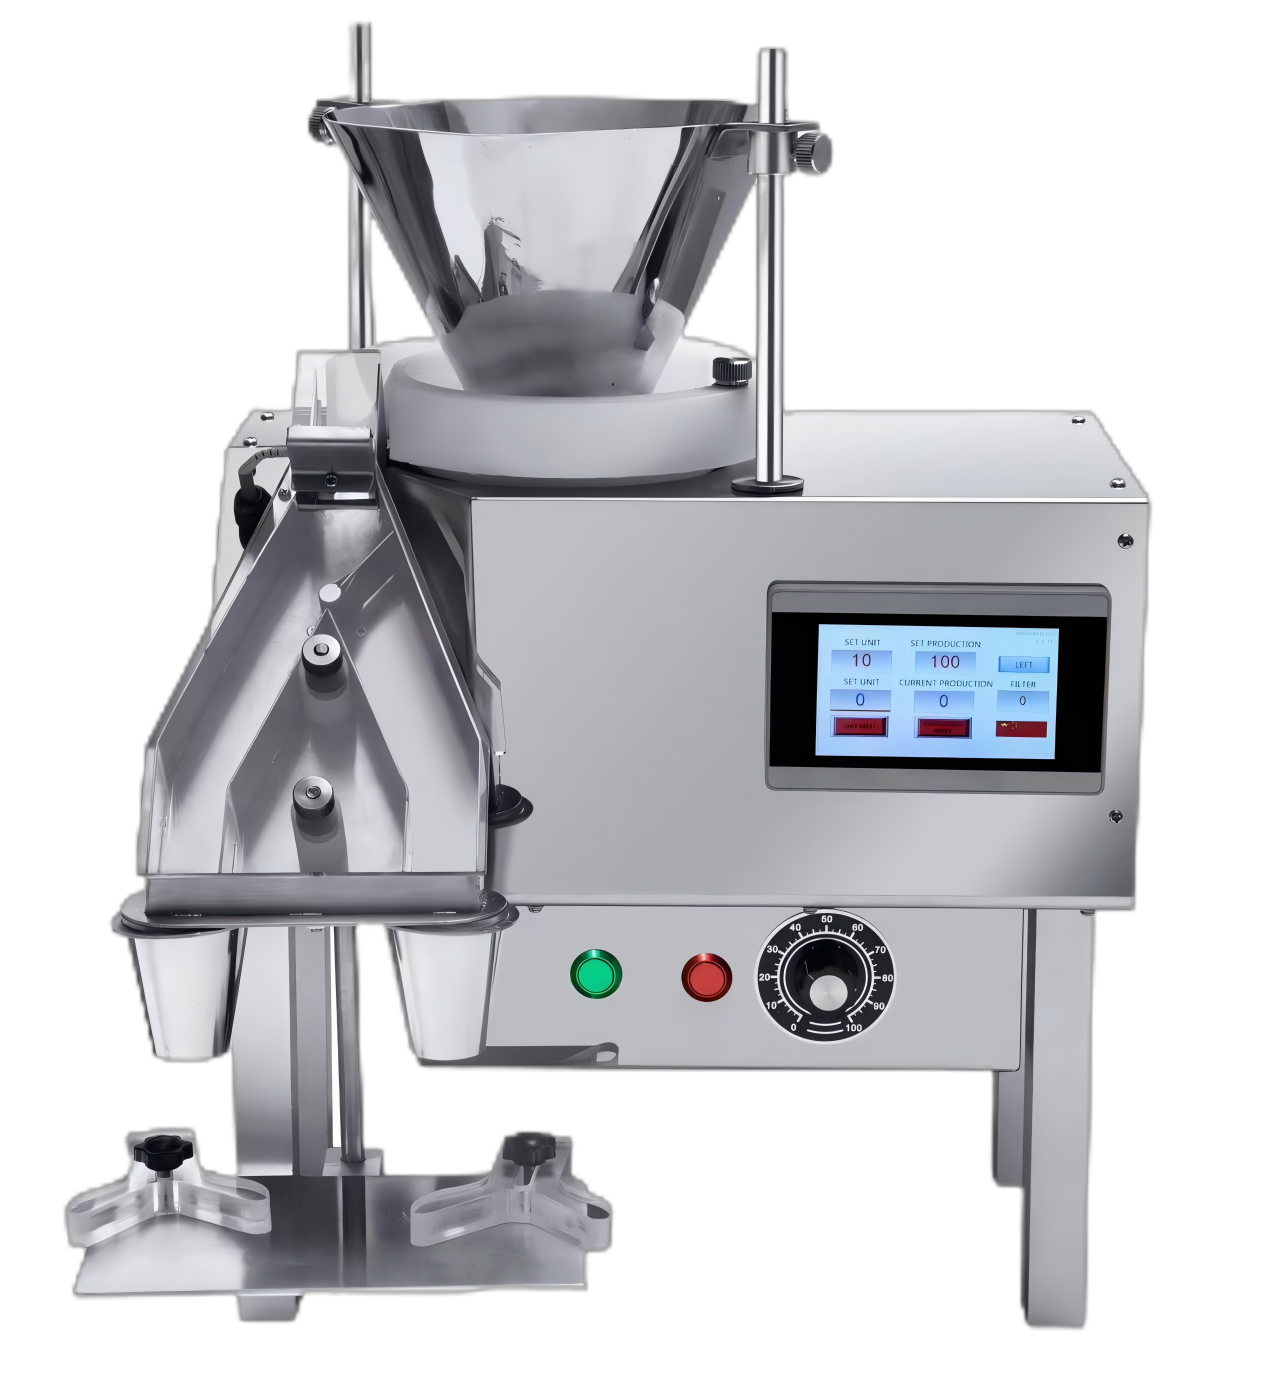
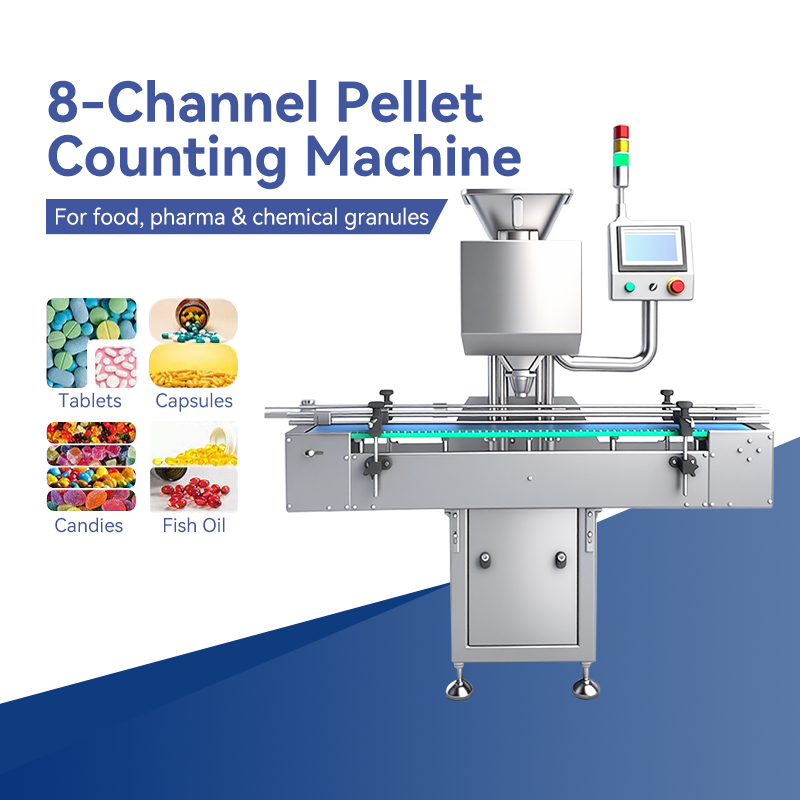
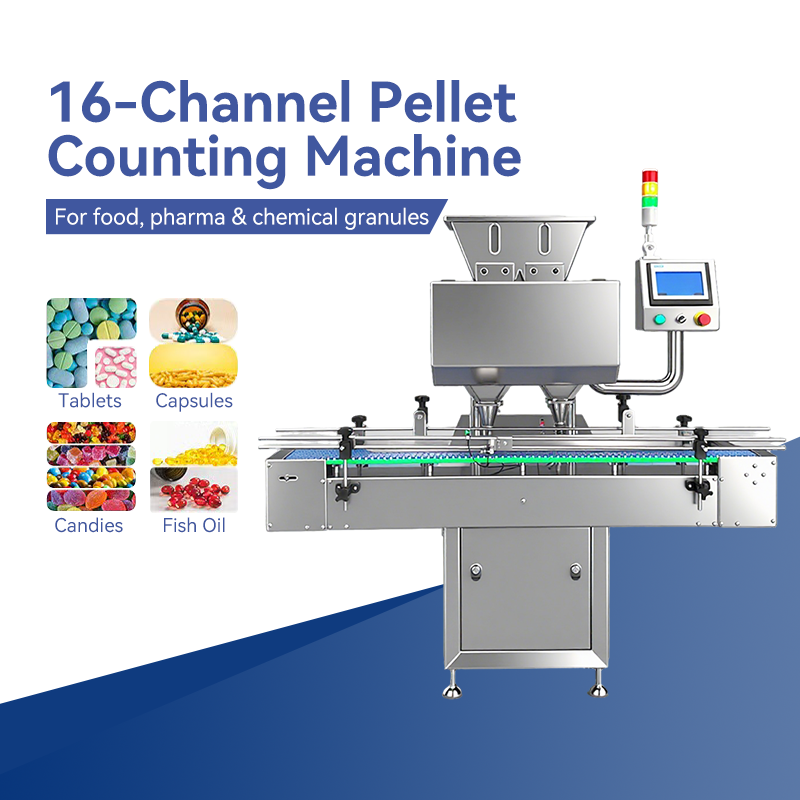
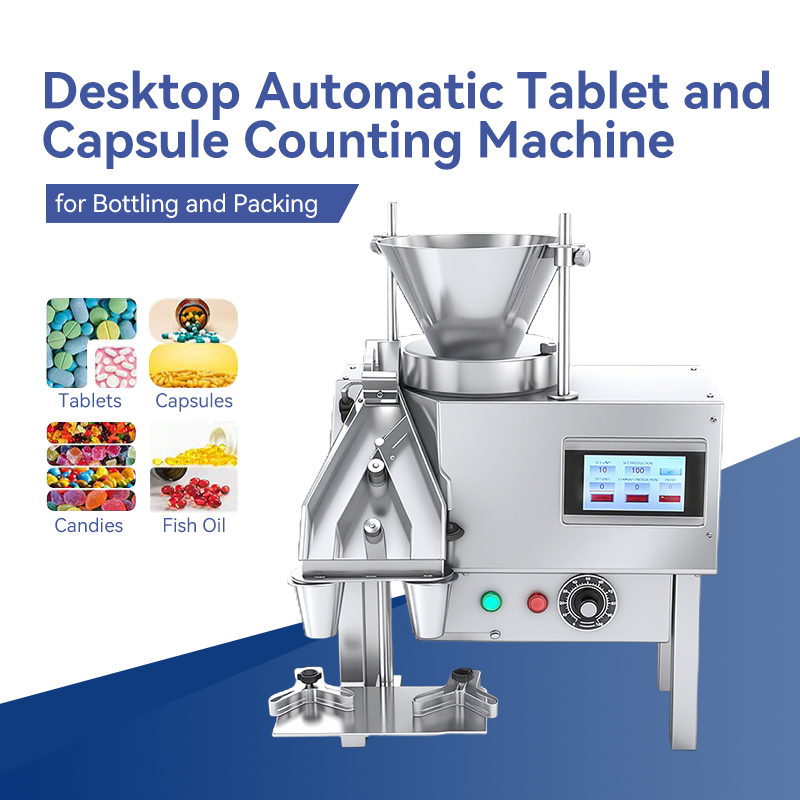
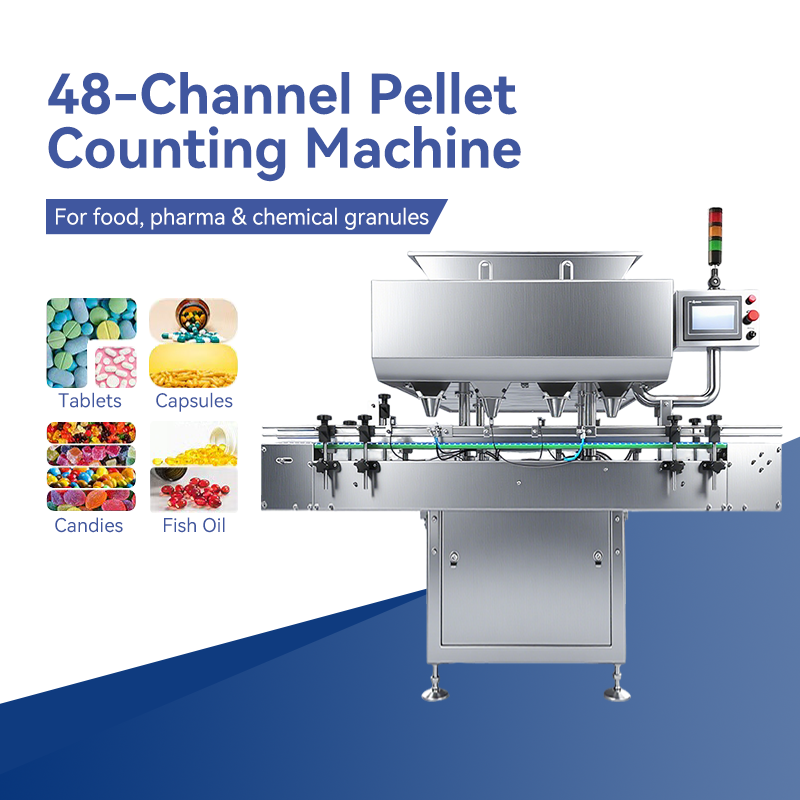
In the highly regulated field of modern pharmaceutical and nutritional supplement production, precision, efficiency, and compliance are not merely goals but indispensable requirements. As a key technology for meeting these core needs, tablet and capsule counting and filling machines have become the core equipment for transforming packaging production lines from potential sources of errors and inefficiency into reliable and efficient operations.
The primary importance of this equipment lies in its ability to ensure absolute precision in counting. Manual operations inherently prone to errors can lead to costly overfilling or underfilling of products, which not only violates strict regulations but also damages brand reputation. By automating operations through high-precision sensors, it ensures that every bottle of product is accurately counted, thereby safeguarding the company's profits and reputation.
Additionally, it is a key driver of operational efficiency. The device can process tens of thousands of units per hour, significantly increasing production throughput, reducing labor costs, and minimizing product waste. This enables manufacturers to easily scale up production, meet tight delivery deadlines, and enhance overall profitability.
Lastly, its design, specifically engineered for compliance, is indispensable. The equipment adheres to Good Manufacturing Practice (GMP) standards, featuring easy-to-clean surfaces and contamination-resistant materials, fundamentally ensuring product integrity. This not only provides convenience but is also a fundamental requirement for any certified production facility.
Essentially, this equipment is far more than a simple packaging function—it is a critical investment in quality control, cost savings, and regulatory compliance, undoubtedly a core asset indispensable to modern production lines.

20
May
20
May
20
May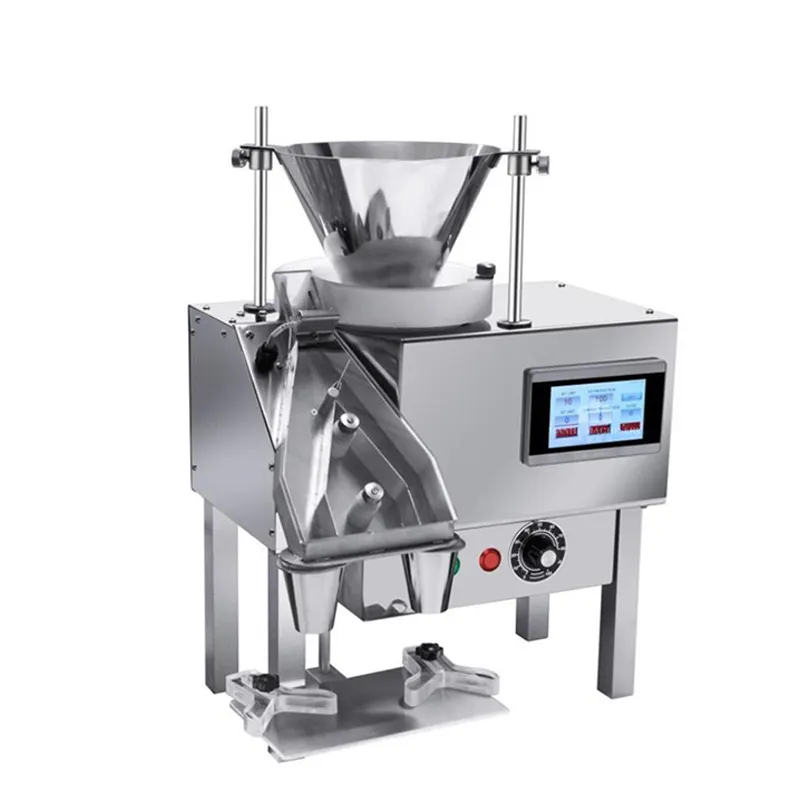
17
Aug
"A Game-Changer for Accuracy. After a near-miss error with a manual count, we invested in this. The peace of mind it provides is worth every penny. Our counts are now perfect every time, and I finally sleep easy knowing our patients are safe."
"Robust and Reliable. We've been running it daily for over a year without a single issue. It's built to withstand the demands of a busy pharmacy. It’s the most dependable piece of equipment we have."