EN


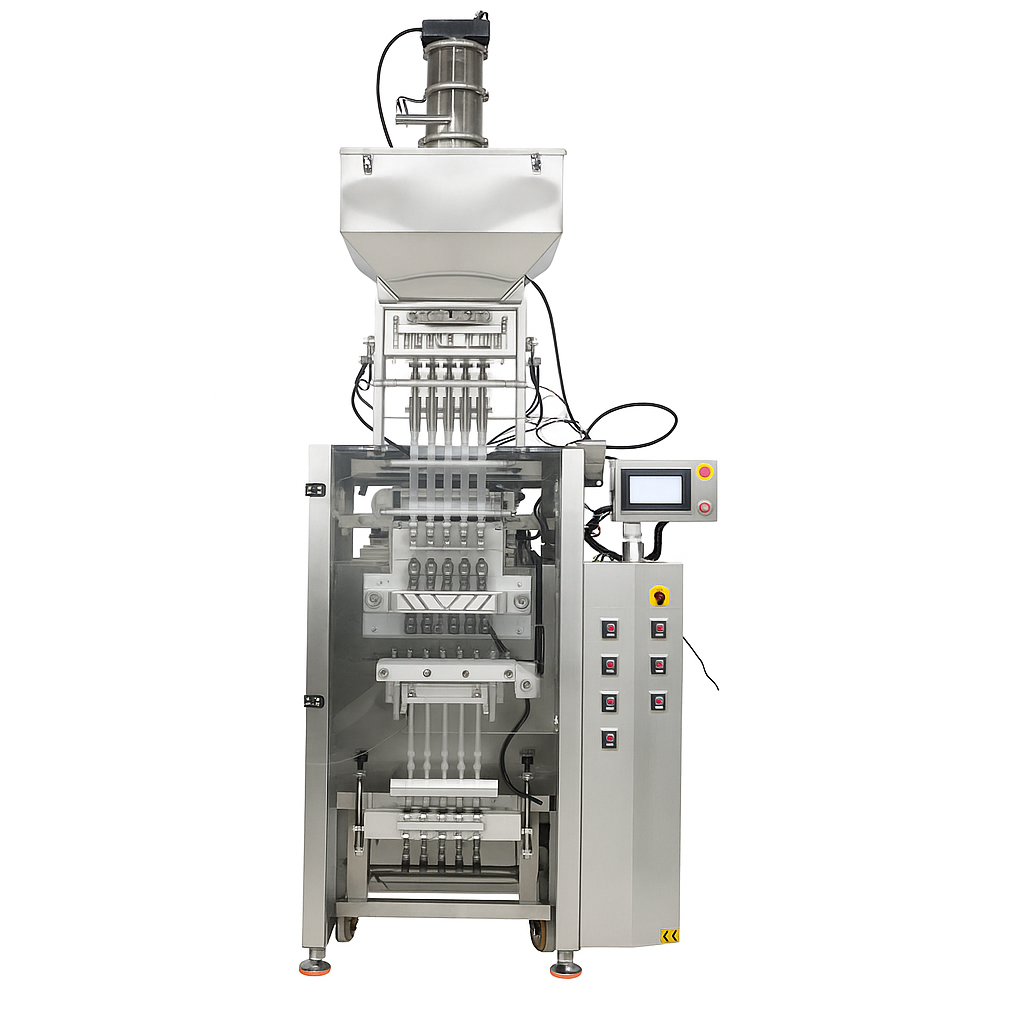
In the modern pharmaceutical, health supplement, and healthcare industries, precision, safety, and efficiency are not merely goals but non-negotiable requirements. It is against this backdrop that tablet packaging machines have evolved from simple devices into the reliable foundation and core of operational scalability. Their importance extends far beyond automation; they represent a critical investment in quality control, regulatory compliance, and brand reputation.
The core significance of tablet packaging machines is first reflected in their unparalleled accuracy and assurance of patient safety. By eliminating the inherent risks of errors in manual counting and packaging through automated operations, they ensure that the number of tablets in each blister pack or medication pouch is precise and error-free, thereby significantly reducing the risk of underdosing or overdosing. This establishes the first line of defense in safeguarding patient safety and drug efficacy. Secondly, in response to stringent global regulations (such as the US FDA 21 CFR Part 11), modern tablet packaging machines are specifically designed to comply with cGMP (current Good Manufacturing Practice). They can precisely print batch numbers, expiration dates, and barcodes on packaging, creating a secure, auditable traceability chain that enables end-to-end traceability from raw materials to the patient's hands. This is critical for quality control and product recalls when necessary.
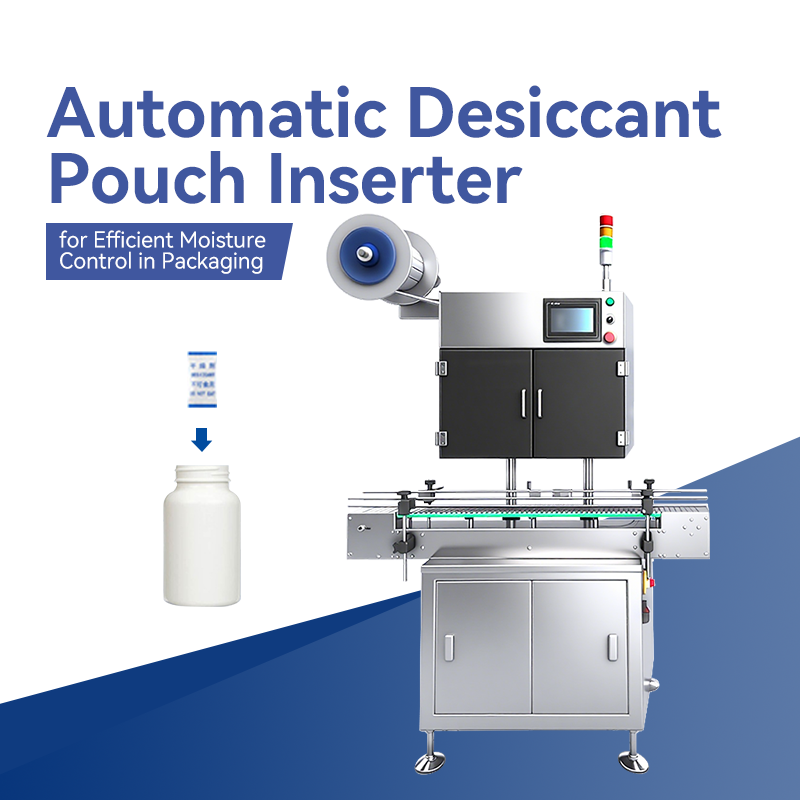
Additionally, this equipment significantly enhances production efficiency and scalability. It compresses tasks that previously required manual teams to complete in hours into minutes, achieving exponential growth in production line speed through automated counting, sorting, and packaging processes. This allows manufacturers to expand production without linearly increasing labor costs or time, directly enhancing profitability and growth potential. In terms of product protection, many tablet packaging machines (especially blister packaging machines) create a sealed environment to protect sensitive medications from moisture, light, and contamination. Combined with the automatic addition of desiccants, this significantly ensures the stability and efficacy of medications throughout their shelf life.
Ultimately, consistent, professional, and tamper-proof packaging directly reflects brand quality. Tablet packaging machines provide a uniform, high-quality appearance for each product unit, fostering strong trust among pharmacists, healthcare providers, and end consumers, thereby reinforcing the company's reputation as a meticulous and reliable manufacturer.

20
May
20
May
20
May
20
May
“Precise and efficient, ideal for small-batch production, with extremely convenient material changeovers.”
“The most reliable equipment on the production line, stable long-term operation, and easy employee training.”