EN


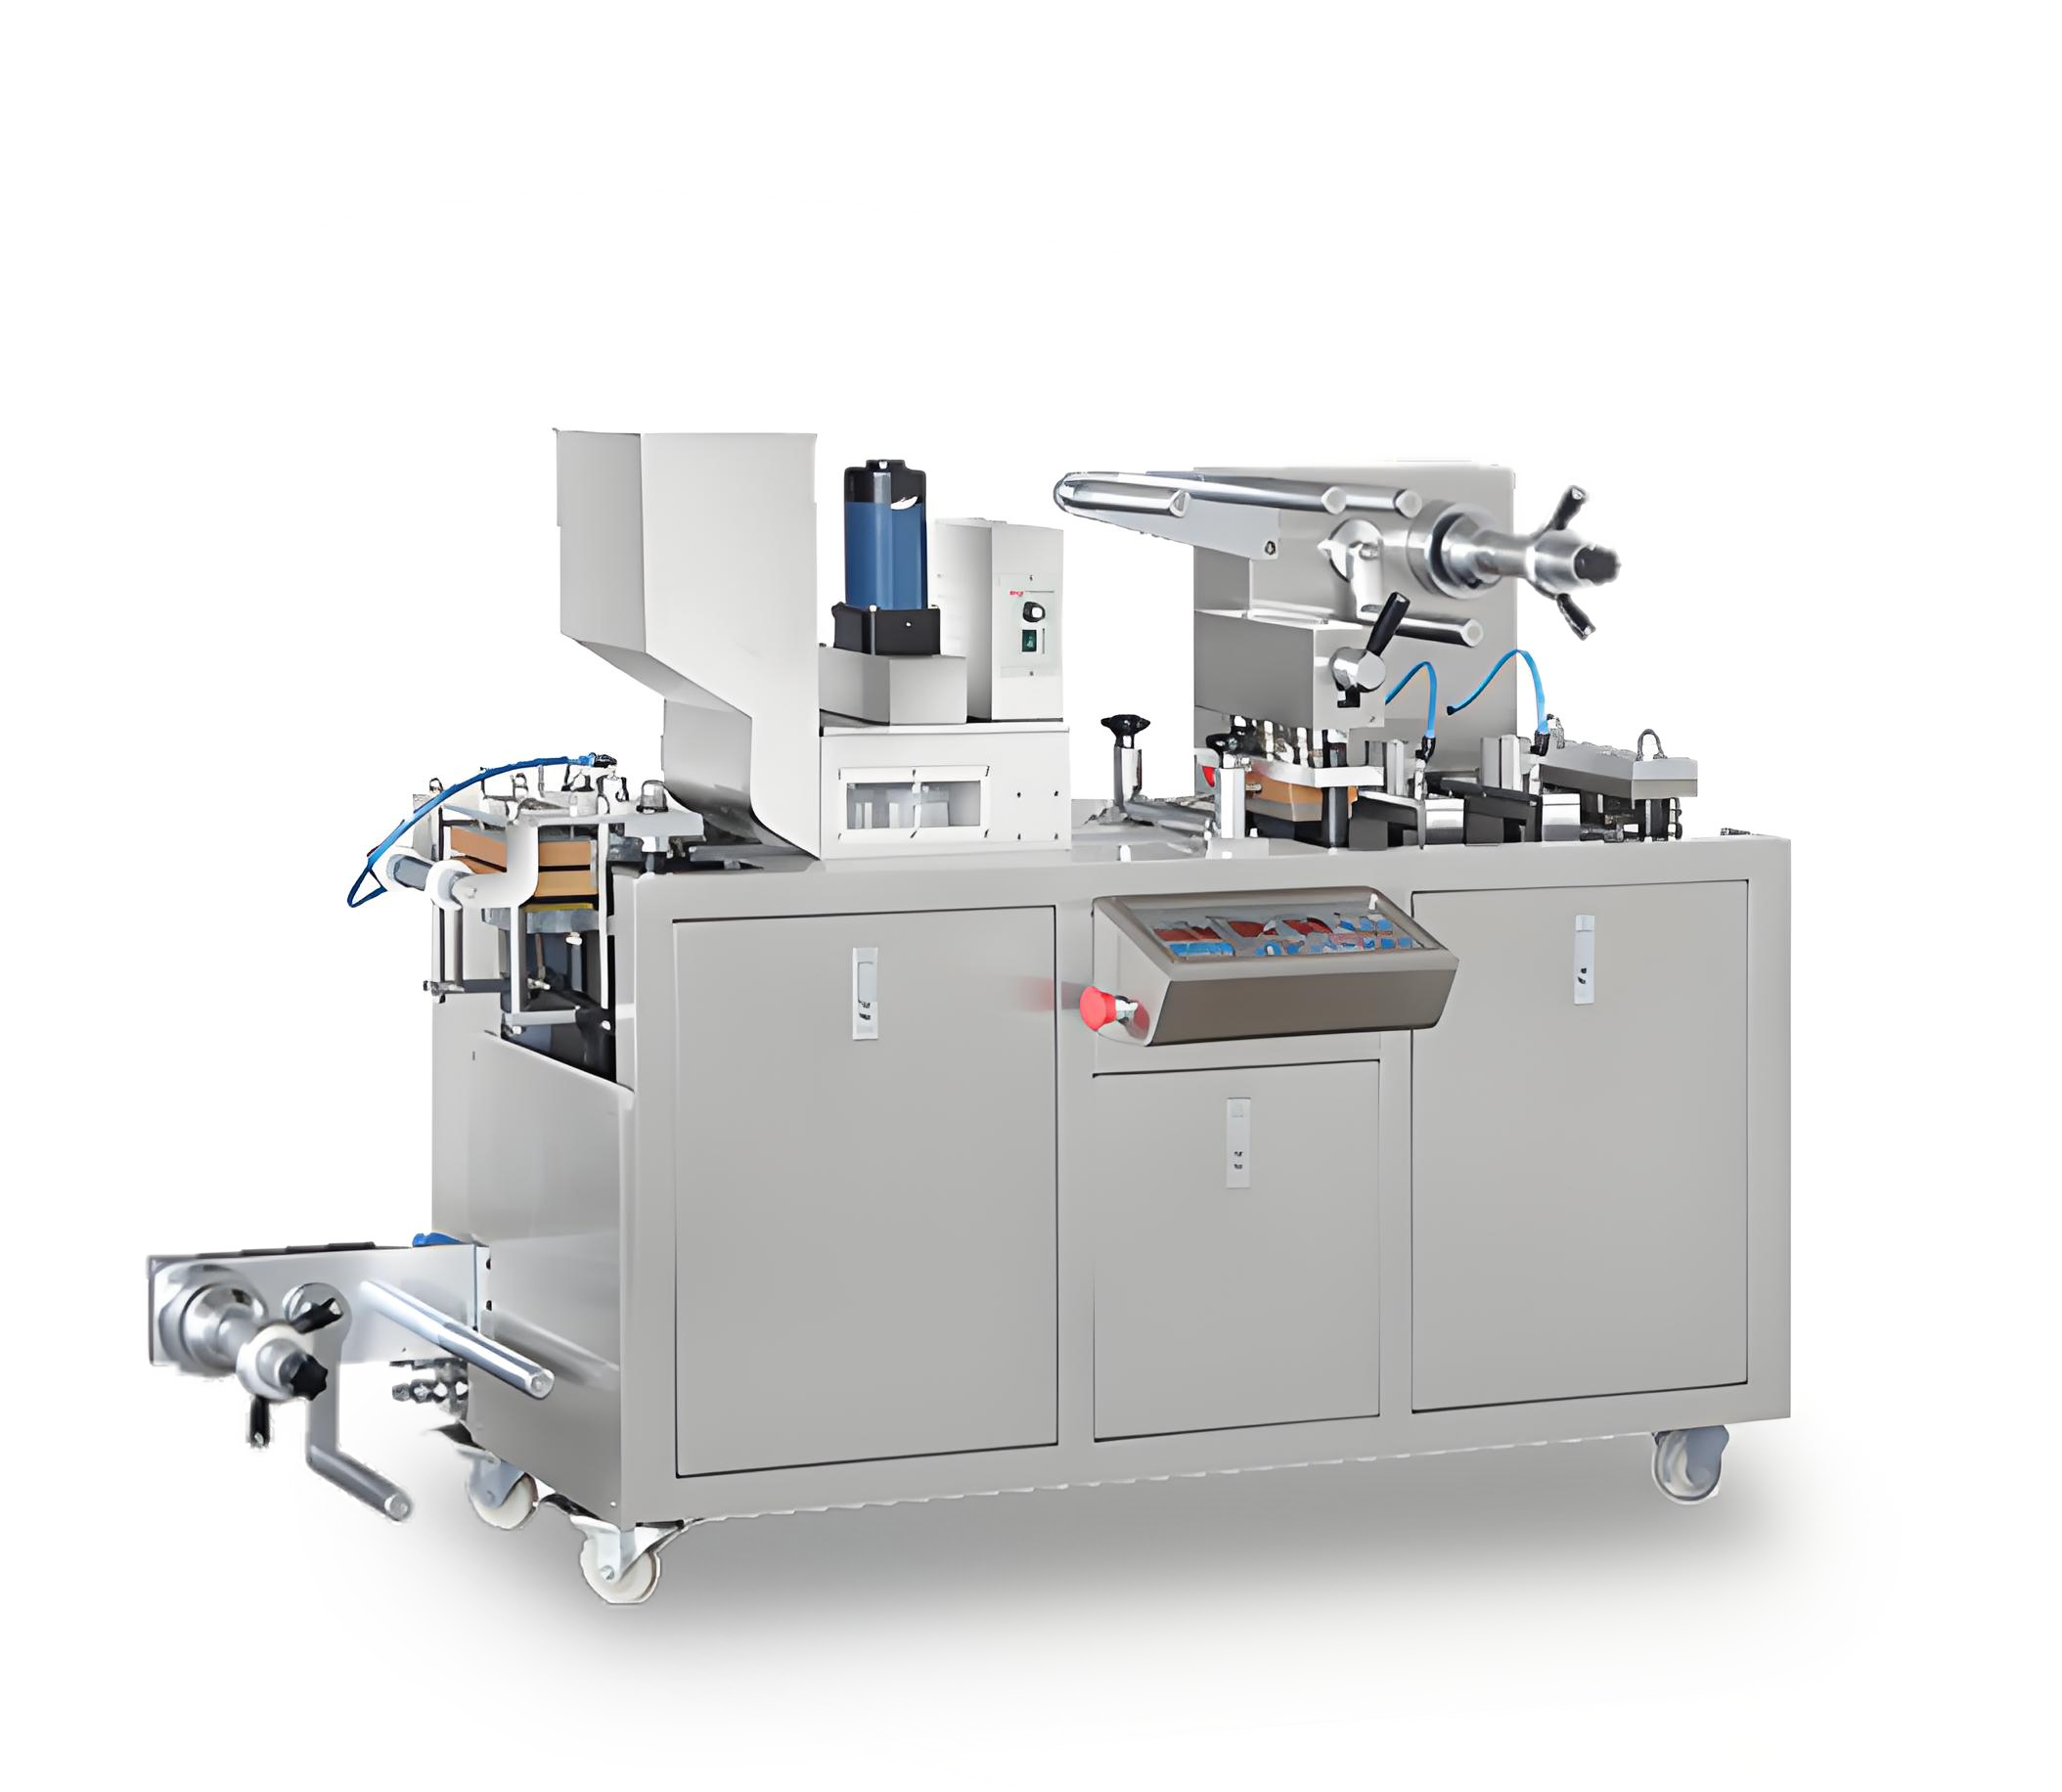
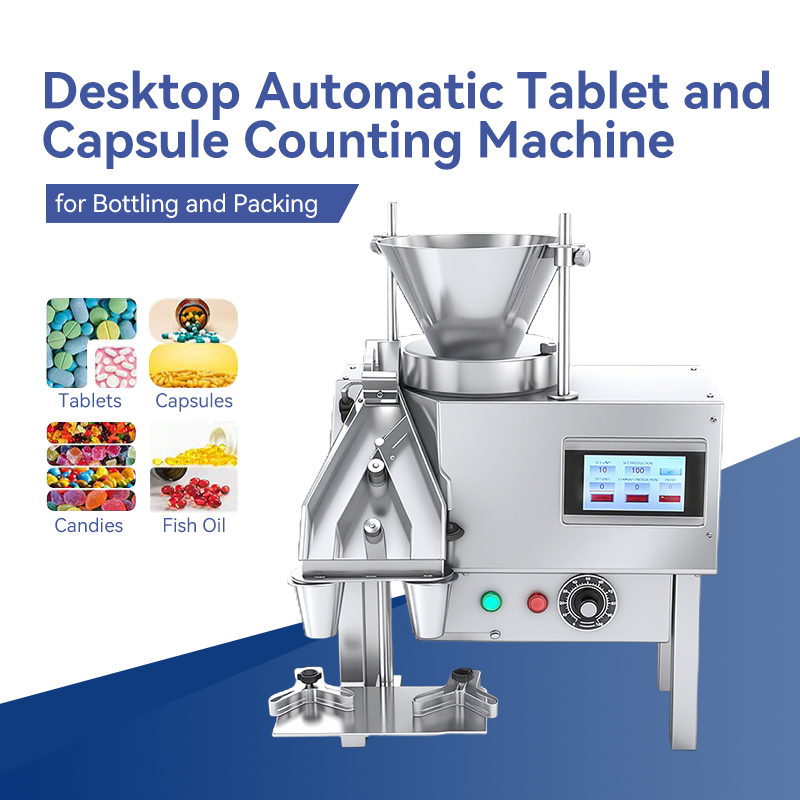
In the modern pharmaceutical and nutritional supplement industry, pill packaging equipment is far more than just simple container filling machinery; it is the cornerstone for ensuring product safety, enhancing operational efficiency, and safeguarding brand reputation. Its primary significance lies in ensuring patient safety and regulatory compliance. Through high-precision automatic counting and filling, this equipment completely eliminates the risks of dosage errors and contamination associated with manual operations. It can also seamlessly integrate tamper-proof sealing, laser coding, and visual inspection systems to ensure that each package is printed with the exact batch number, expiration date, and serialized coding required by regulatory agencies such as the U.S. FDA's DSCSA regulations.
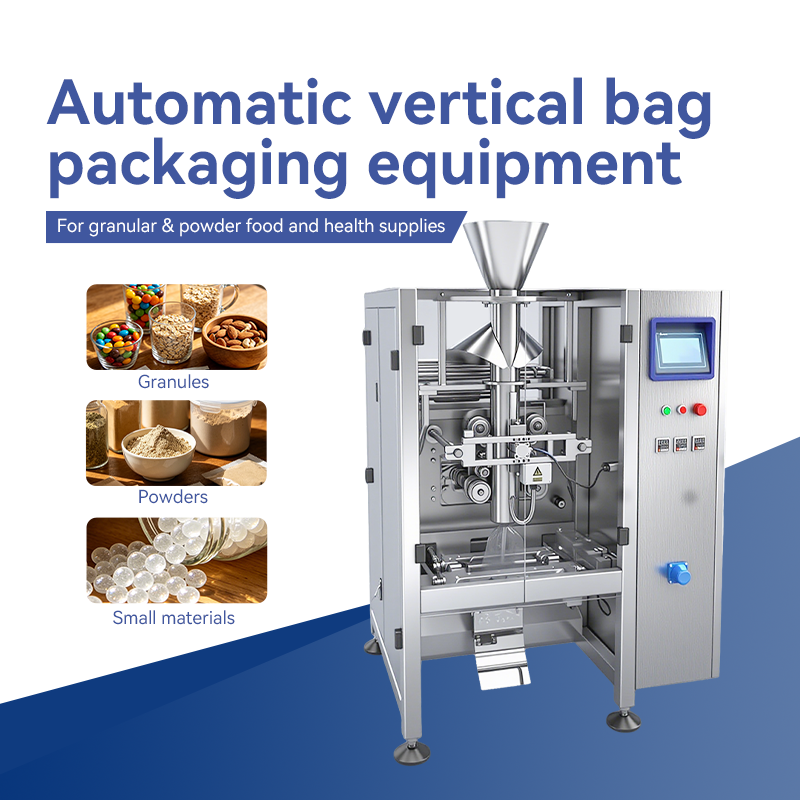
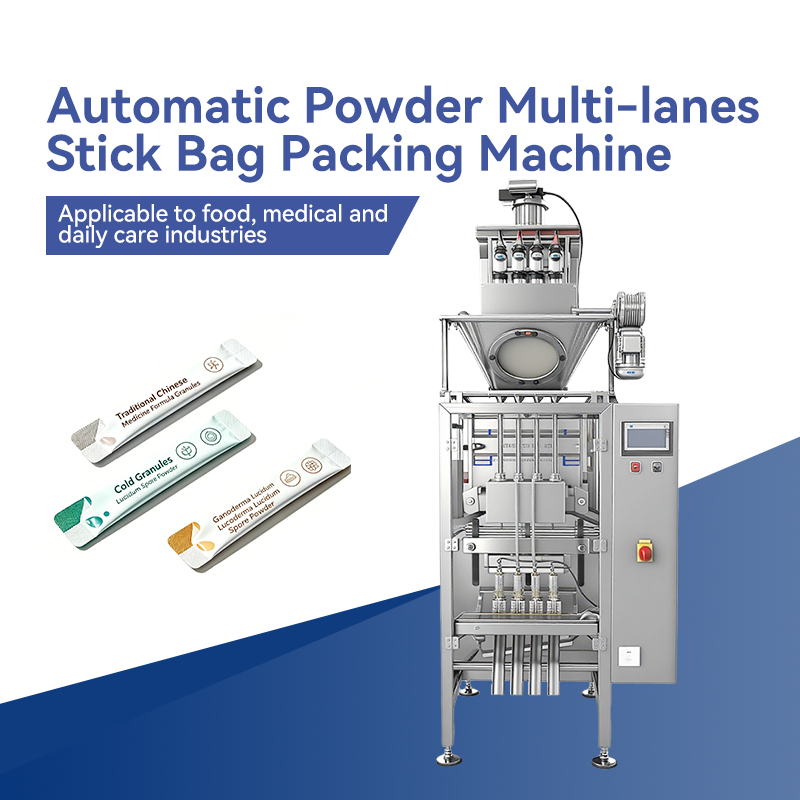
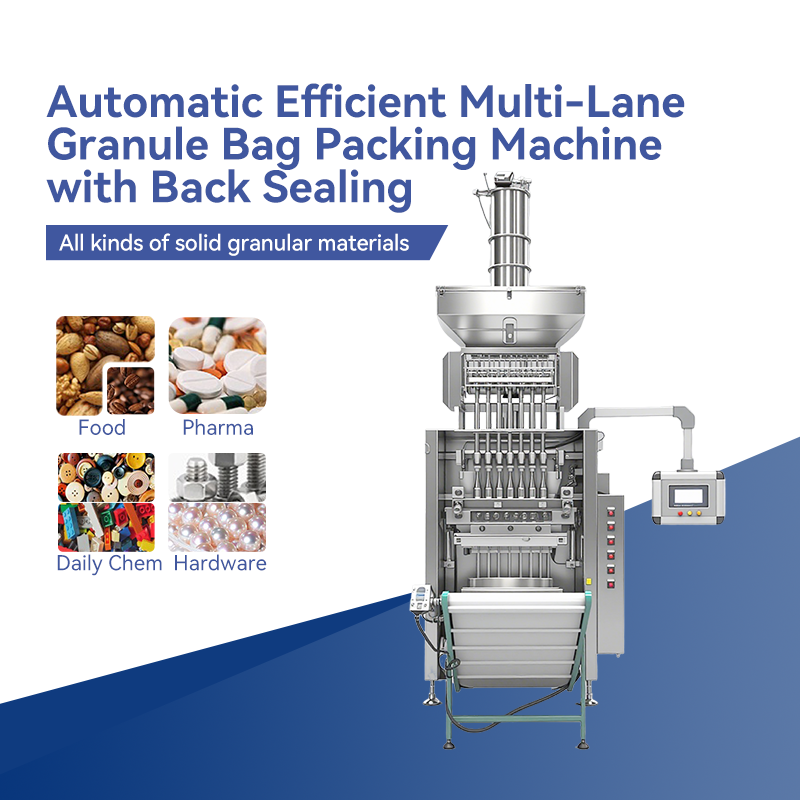
Secondly, such equipment serves as a powerful engine driving operational efficiency and cost control. Automated production lines can operate at speeds of thousands of units per hour, far exceeding human limits, enabling companies to easily meet market demand while optimizing the allocation of valuable human resources to higher-value roles such as quality control and process improvement. Precision mechanical control also minimizes losses caused by overfilling or waste of packaging materials.
Additionally, pill packaging equipment plays an irreplaceable role in protecting product integrity and stability. For example, blister packaging machines use high-barrier materials to form sealed chambers, effectively isolating moisture and oxygen; while bottling lines can integrate nitrogen purging systems, significantly extending the shelf life of medications.
Finally, it directly impacts brand image and consumer trust. Every package produced by the equipment features a professional, uniform, and aesthetically pleasing appearance, serving as a tangible manifestation of the brand's commitment to quality. Additionally, patient compliance features supported by the equipment (such as weekly blister boards and easy-open caps) enhance the medication experience, further strengthening user loyalty to the brand.
In summary, investing in advanced tablet packaging equipment is a strategic decision that impacts product lifecycle, operational efficiency, and market competitiveness, serving as the ultimate guarantee for safely and reliably delivering high-quality products to every patient who relies on them.

20
May
20
May
20
May
20
May
“Precise and efficient, ideal for small-batch production, with extremely convenient material changeovers.”
“The most reliable equipment on the production line, stable long-term operation, and easy employee training.”