EN


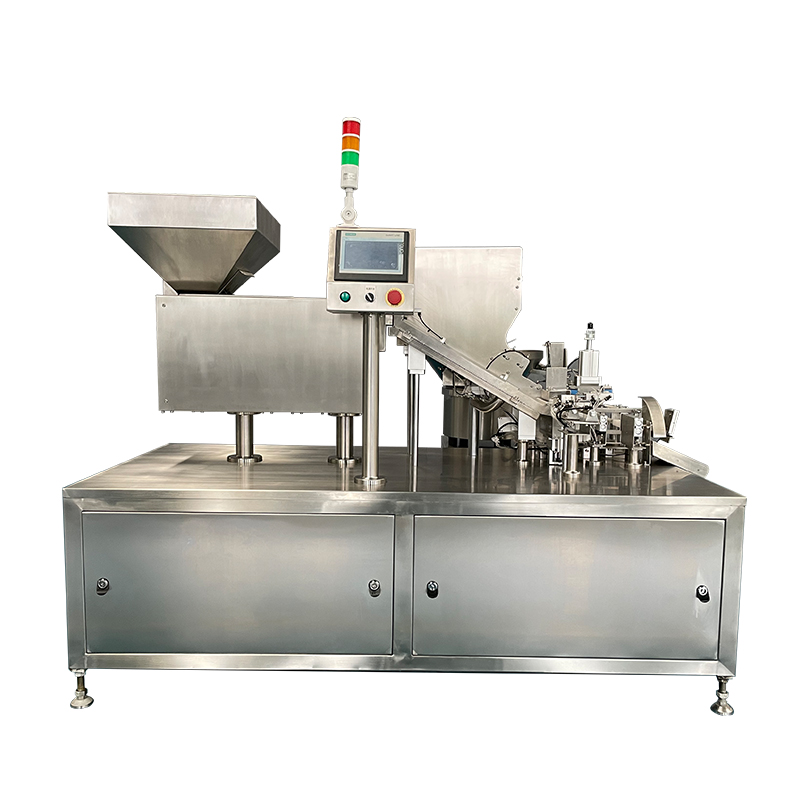
In the pharmaceutical industry, fully automated capsule filling equipment can meet the growing demand for generic drugs and customized medications, supporting a precise transition from small-scale R&D production to large-scale commercial manufacturing. It complies with stringent international standards such as GMP and FDA regulations, ensuring traceability and safety for each batch of products, and effectively handling complex formulations including powders, granules, and microtablets.
In the rapidly growing field of nutritional supplements and the health industry, capsule manufacturing technology demonstrates significant market agility—companies can swiftly respond to consumer trends, producing a diverse range of products including vitamins, probiotics, and herbal supplements. Through flexible capsule specifications and color customization, they can create unique brand identities while leveraging in-house production to effectively control costs and ensure formulation quality.
Additionally, in the veterinary pharmaceutical sector, capsule machines can precisely prepare antibiotics, vitamins, and antiparasitic drugs tailored to different animal sizes, ensuring accurate and safe administration while avoiding the inconvenience of liquid formulations. The equipment has also opened up many emerging niche markets, such as capsules for oral beauty products (collagen, biotin, etc.) under the “cosmeceutical” category, as well as modern production of traditional herbs and Ayurvedic products, enabling ancient therapies to reach global markets through standardized dosages. Research institutions, CROs, and compounding pharmacies also rely on these devices for clinical trials and small-batch custom production.
Investing in pharmaceutical capsule manufacturing equipment is not only focused on current needs but also a strategic layout for the future—it empowers companies to rapidly expand their product lines, reduce reliance on third-party contract manufacturing, enhance supply chain autonomy, and shorten product time-to-market, laying the foundation for entering international markets. Overall, the application prospects for capsule manufacturing equipment continue to grow and diversify, offering not only advanced technology but also the core capabilities to drive innovation, growth, and leadership in the global health market.

20
May
20
May
20
May
20
May
“The accuracy far exceeded our expectations and completely solved the dosage stability issues we had with small-batch formulations.”
“It performs excellently in handling highly active powders, has a complete verification process, and meets the strict requirements of our cGMP production line.”