EN


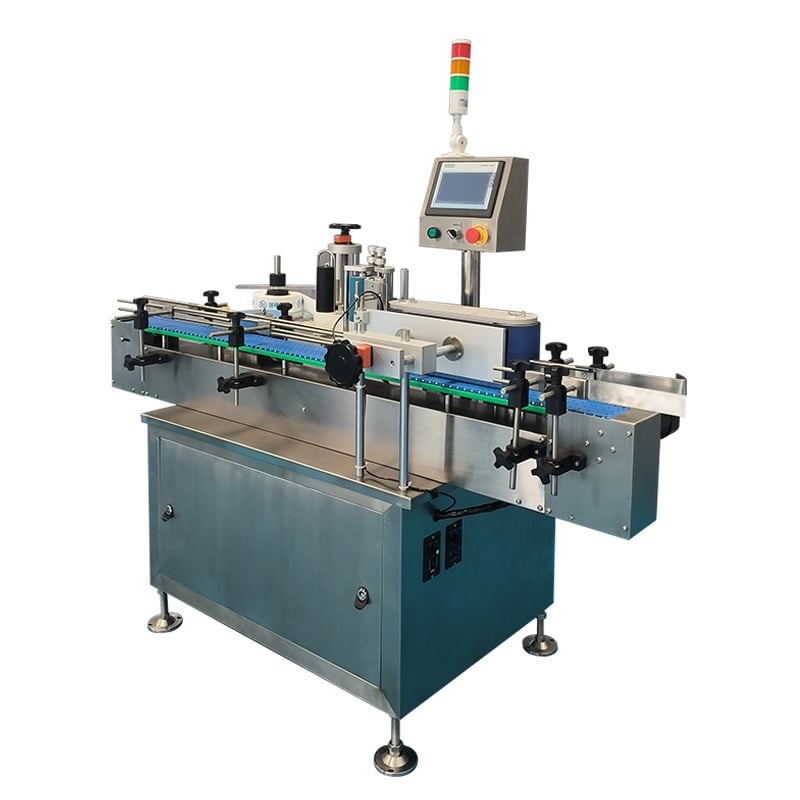
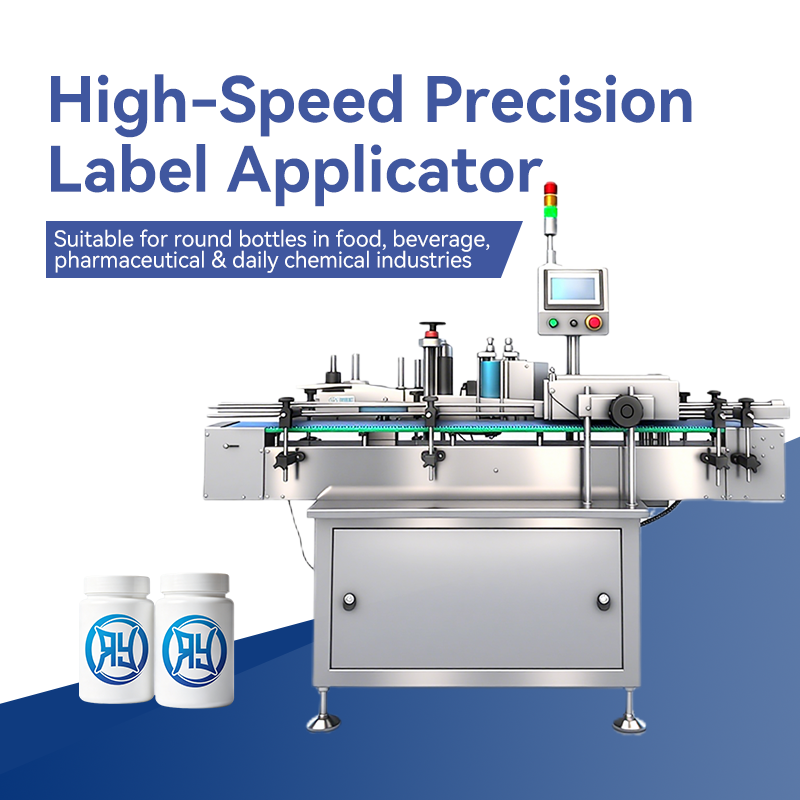
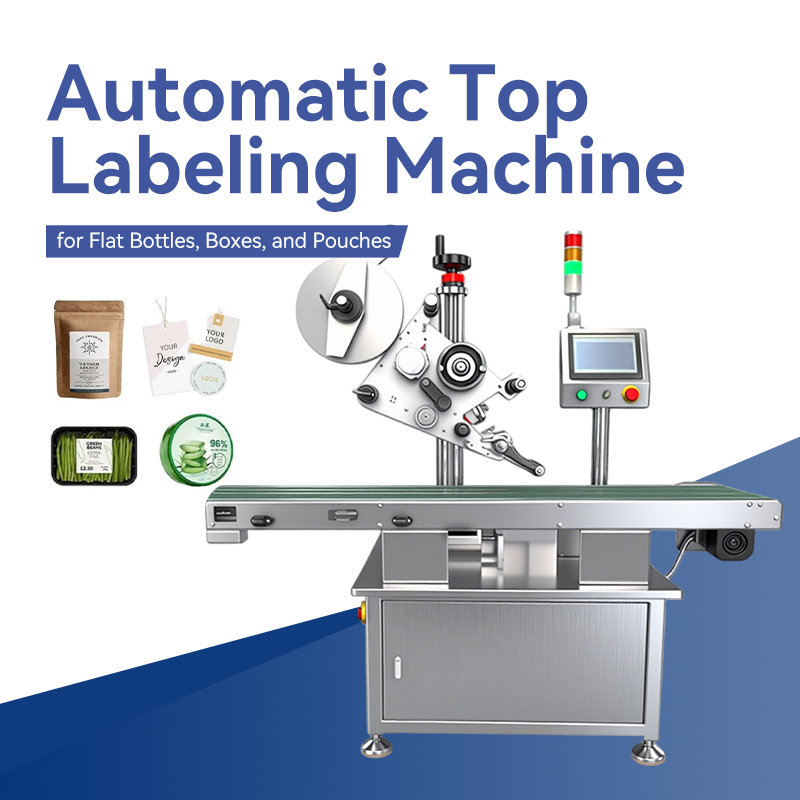
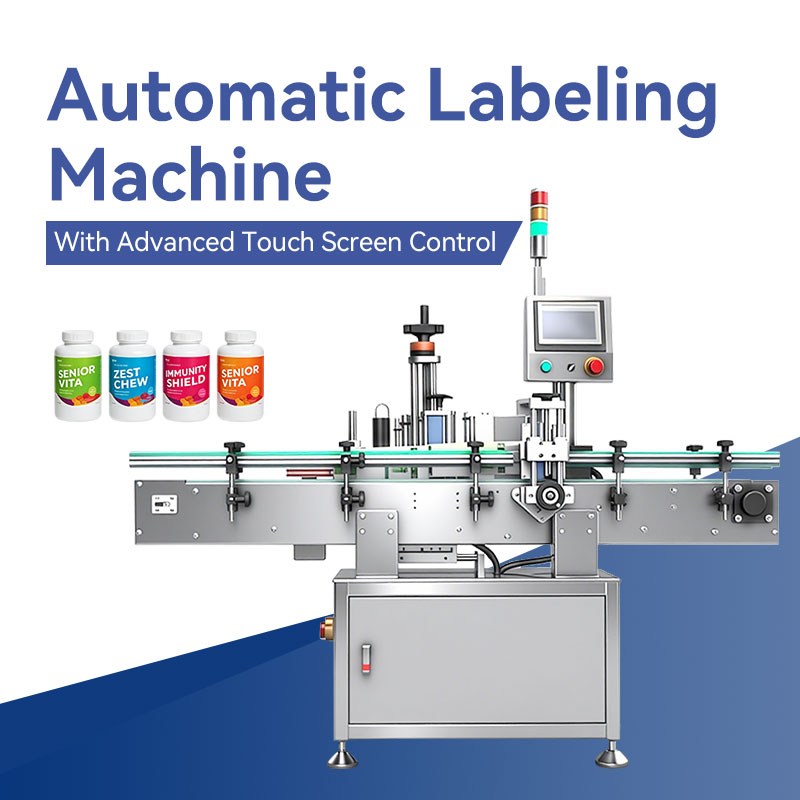
In modern industrial production, tube labeling machines are core equipment for enhancing production line efficiency and ensuring precise, compliant labeling. Their applications are extremely broad, spanning numerous industries with stringent packaging labeling requirements. In the pharmaceutical and medical sectors, these machines are indispensable for labeling products like ointments, medical gels, and sterile sample tubes. They must meet stringent regulatory standards such as FDA requirements, ensuring clear identification of batch codes and scannable barcodes (e.g., UDI/GS1) to safeguard patient safety. The cosmetics and personal care industry similarly relies heavily on these machines. Labels are key to product branding and shelf appeal, requiring machines to ensure bubble-free, wrinkle-free, and perfectly aligned application on containers like skincare jars, toothpaste tubes, and lipstick tubes to maintain a premium, aesthetically pleasing finish.
Additionally, in the food and beverage sector, tube labeling machines are used for products like condiment tubes, yogurt containers, and beverage concentrate tubes. Labels must be moisture-resistant and cold-storage-proof while clearly displaying nutritional information and expiration dates to meet food safety standards. For chemical and industrial products, equipment must withstand harsh environments, applying exceptionally durable, chemically resistant labels to containers holding adhesives, lubricants, sealants, and similar products. This ensures safety warnings and operating instructions remain permanently affixed and legible. Finally, in the cross-sector of nutritional supplements and health products, labeling machines must balance regulatory compliance for ingredient labeling with consumer-attractive packaging design. They are widely deployed on high-speed packaging lines for products like vitamin gummies and energy bars.

20
May
20
May
20
May
20
May
“Efficiency has improved significantly, and the packaging looks much more professional.”
“Stable operation and high precision, the main equipment on the production line.”