EN


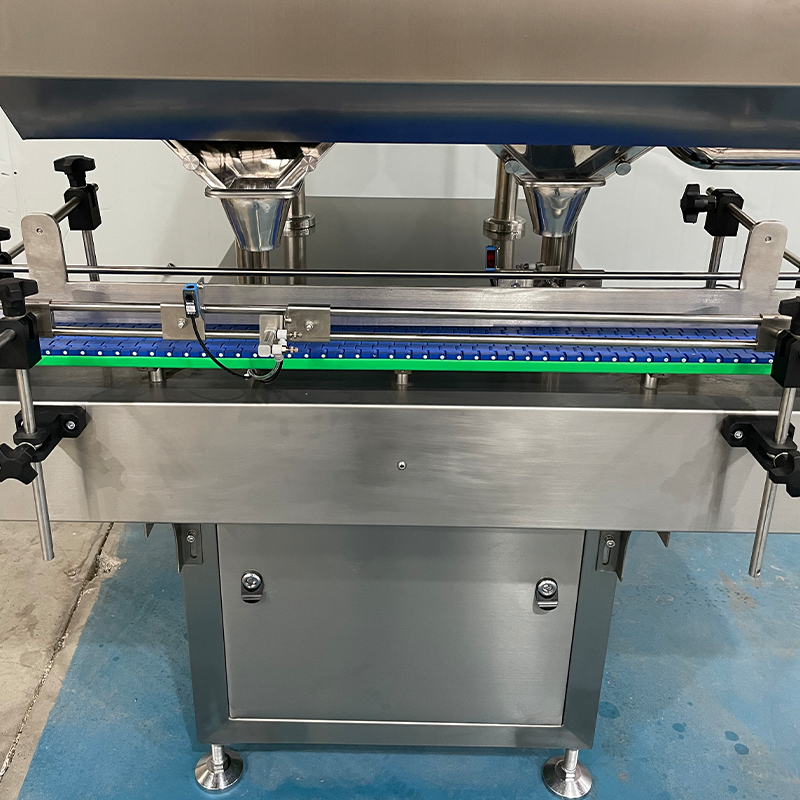
The Application Prospects of Pharmaceutical Tablet Counters
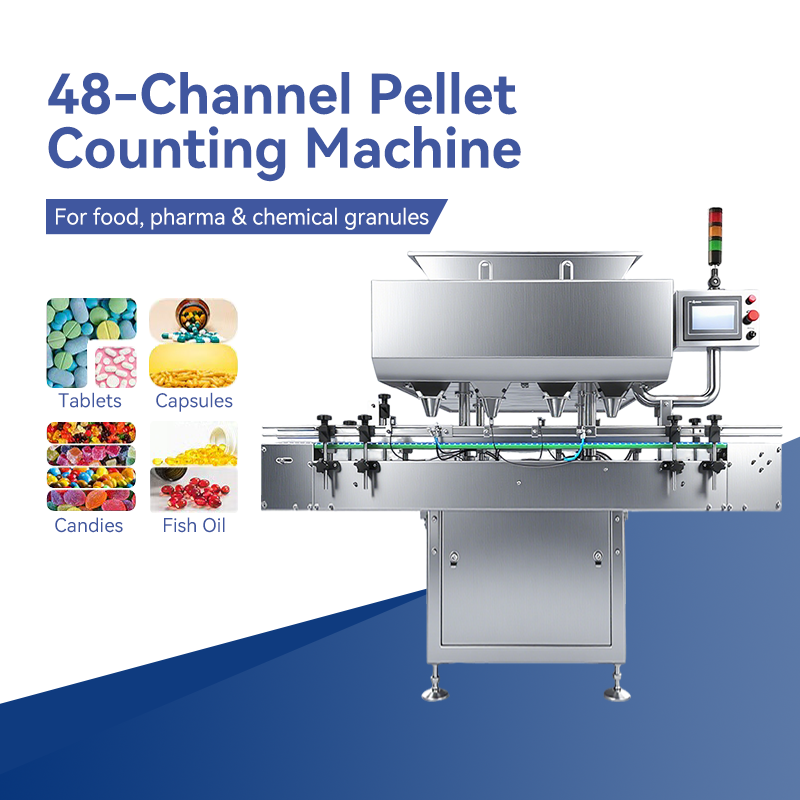
As a critical piece of equipment in the modern pharmaceutical and medical industries, the application prospects of pharmaceutical tablet counters are continuously expanding alongside technological advancements and evolving industry demands. This device is not only used for accurately counting solid oral dosage forms (such as tablets, capsules, soft capsules, and lozenges) but also demonstrates significant development potential across multiple fields.
On pharmaceutical production lines, tablet counters have become essential tools in high-speed packaging and filling processes, enabling precise filling of medicine bottles at extremely high speeds to ensure that each batch of products meets the dosage requirements specified on the label. Meanwhile, in pharmacies and medication distribution processes, the use of tablet counters significantly reduces human operational errors, enhances patient medication safety, and allows pharmacists to devote more time to patient care, thereby optimizing the overall allocation of medical resources.
The application of tablet counters is not limited to traditional pharmaceutical fields. With the rise of personalized medicine, they are playing an increasingly important role in drug research and clinical trials. For example, when configuring customized drugs tailored to specific genetic compositions or conditions, tablet counters can precisely allocate multiple active drug components, ensuring individualized dosing and treatment efficacy. Additionally, in the nutritional supplement and cosmetics industries, this equipment is widely used to handle products of different shapes and sizes, helping relevant companies achieve large-scale production while ensuring product quality consistency.
The veterinary field and pet healthcare market have also become important application scenarios for tablet counters. Accurate drug dosing is critical to animal health, and tablet counters efficiently support the entire process from clinic-level distribution to large-scale animal drug production. On the other hand, as global drug serialization and tracking regulations (such as the U.S. DSCSA) become increasingly stringent, the combination of tablet counters with serialization software and printing devices provides pharmaceutical companies with a comprehensive compliance solution, ensuring transparency and traceability from production to the patient.
The rise of Industry 4.0 and smart factories has further expanded the functional boundaries of tablet counters. Modern tablet counters feature IoT connectivity, cloud data recording, and real-time monitoring, making them data nodes in smart factories. They can provide real-time information on production output, equipment efficiency, and even issue predictive maintenance alerts. This data integrates with enterprise ERP and MES systems, enabling seamless connectivity for inventory management, production automation, and operational intelligence.
In summary, the application prospects of pharmaceutical tablet counters are closely linked to the healthcare industry's trend toward personalization, digitization, and stringent quality control. Investing in advanced tablet counting technology not only reduces errors and lowers costs but also helps companies comply with regulatory requirements, scale up production, and ultimately gain a competitive edge in the rapidly evolving healthcare market. Whether in R&D laboratories, custom pharmacies, or large-scale production facilities, tablet counters are essential tools for achieving safe, efficient, and future-oriented operations.

20
May
20
May
20
May
20
May
"A Game-Changer for Accuracy. After a near-miss error with a manual count, we invested in this. The peace of mind it provides is worth every penny. Our counts are now perfect every time, and I finally sleep easy knowing our patients are safe."
"Robust and Reliable. We've been running it daily for over a year without a single issue. It's built to withstand the demands of a busy pharmacy. It’s the most dependable piece of equipment we have."