EN


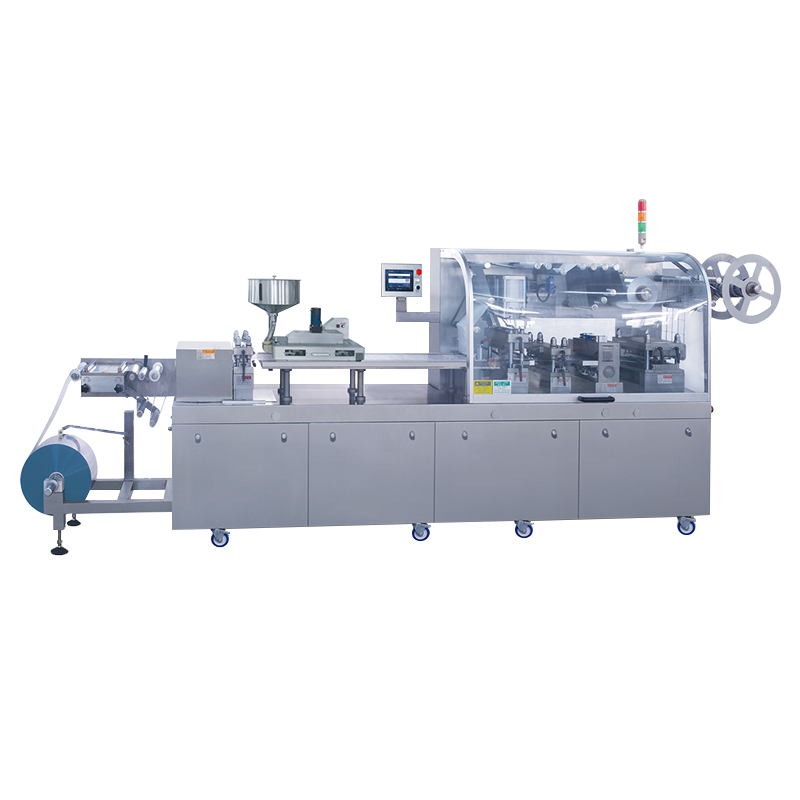
The strategic significance of modern capsule packaging machines extends far beyond the realm of simple equipment; they have become a core investment in ensuring product quality, enhancing production efficiency, and maintaining brand reputation. For the pharmaceutical, health supplement, vitamin, and dietary supplement industries, its importance is evident across multiple critical dimensions. First, it ensures uncompromising dose accuracy and integrity, achieving precision counting rates exceeding 99.9%, thereby completely eliminating human error. This fundamentally safeguards medication safety and meets stringent FDA and GMP regulatory compliance requirements. Second, the equipment achieves a significant leap in production efficiency and scalability through high automation, capable of operating at speeds of hundreds or even thousands of capsules per minute, enabling companies to quickly respond to growing market demand without significantly increasing labor costs.
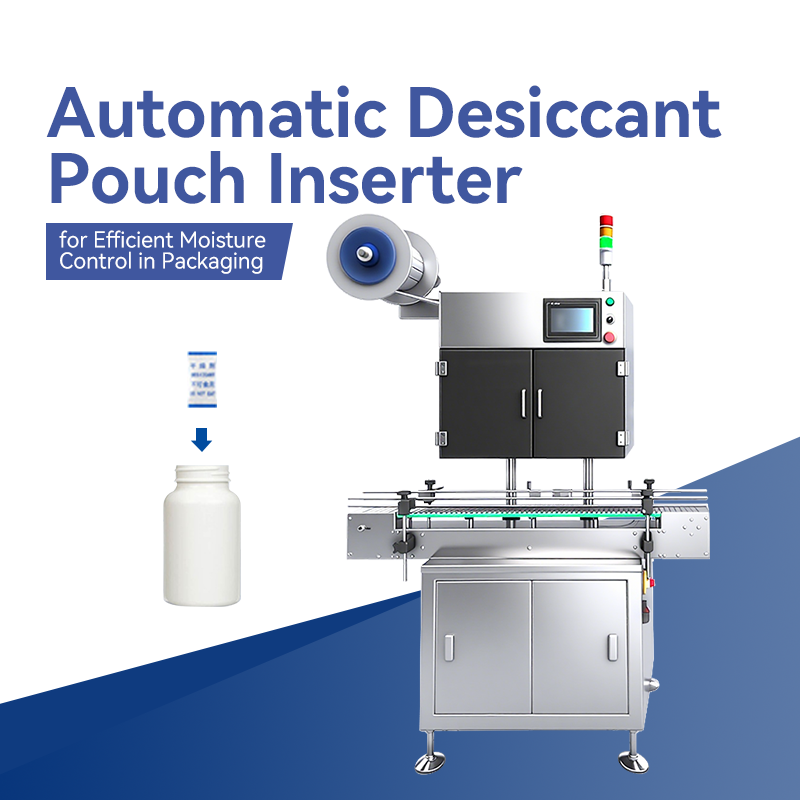
Additionally, the capsule packaging machine forms a reliable airtight seal, effectively resisting environmental factors such as moisture and oxygen, extending product shelf life and maintaining its efficacy and stability. Furthermore, the professional, aesthetically pleasing packaging it produces, complete with anti-counterfeiting features, significantly enhances consumer trust in the brand and market recognition. Finally, the advanced equipment integrates traceability functionality, automatically printing batch numbers, expiration dates, and barcodes to provide full lifecycle traceability for products, streamline audit processes, and ensure comprehensive compliance in globally stringent regulatory environments.

20
May
20
May
20
May
20
May
“Precise and efficient, ideal for small-batch production, with extremely convenient material changeovers.”
“The most reliable equipment on the production line, stable long-term operation, and easy employee training.”