EN


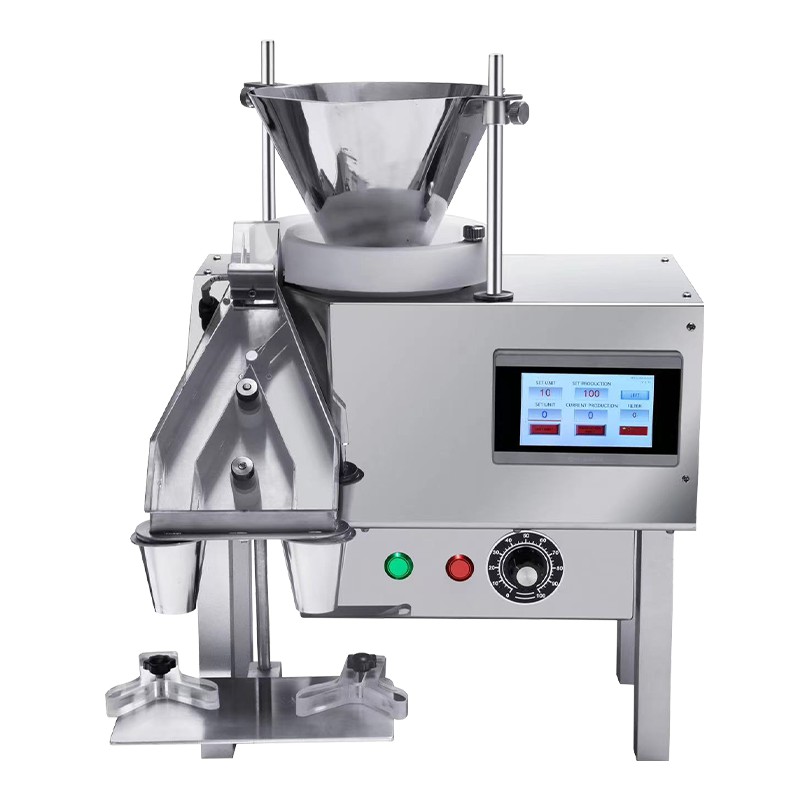
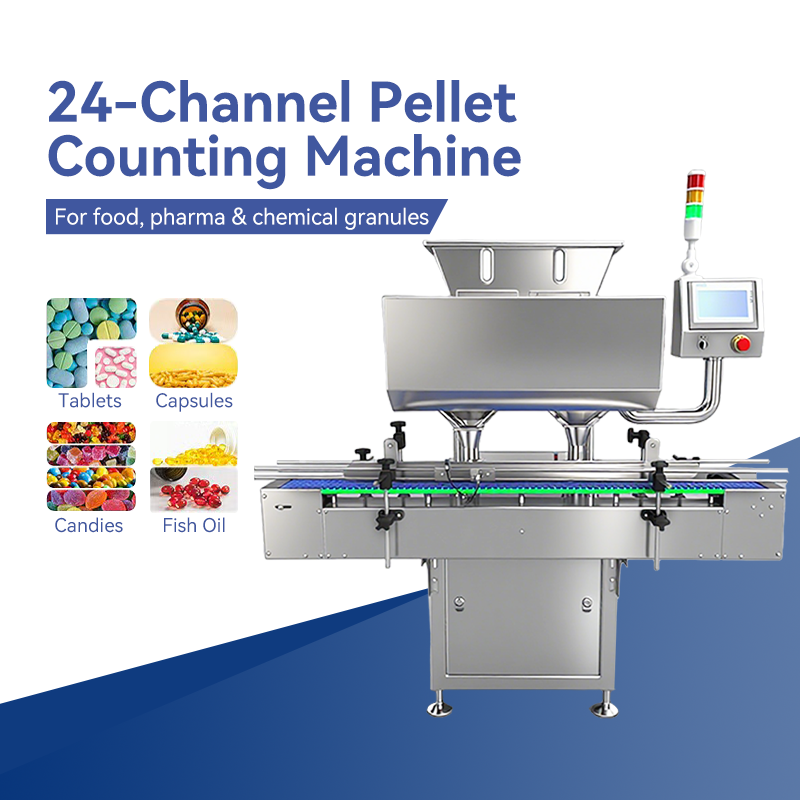
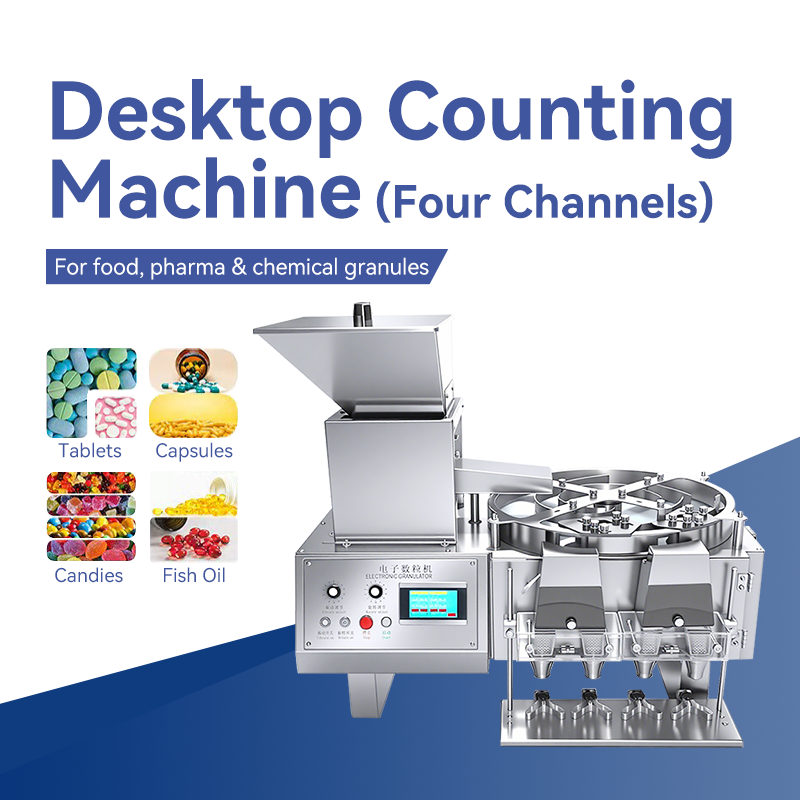
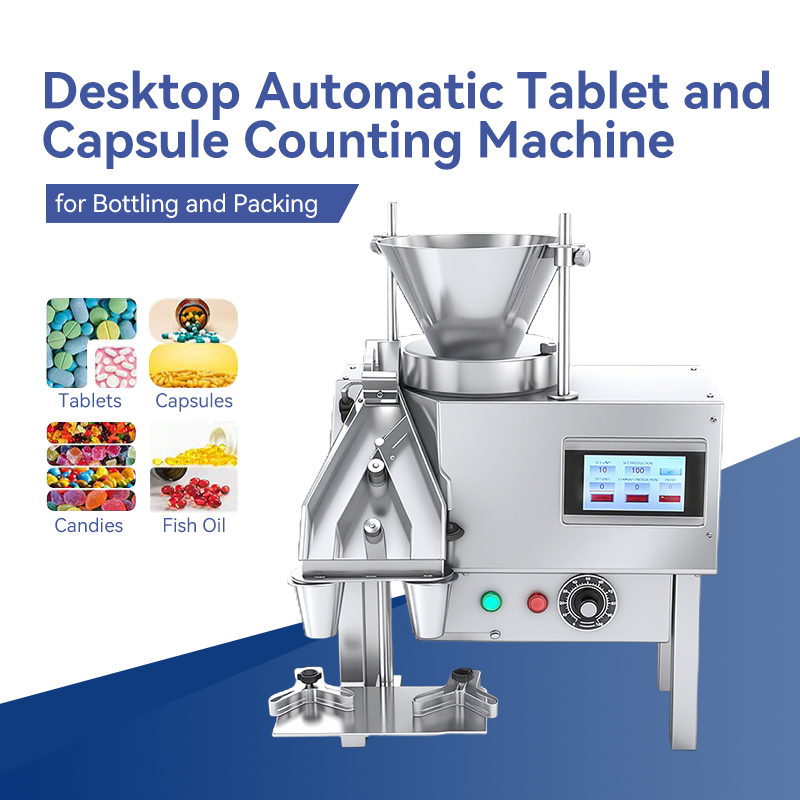
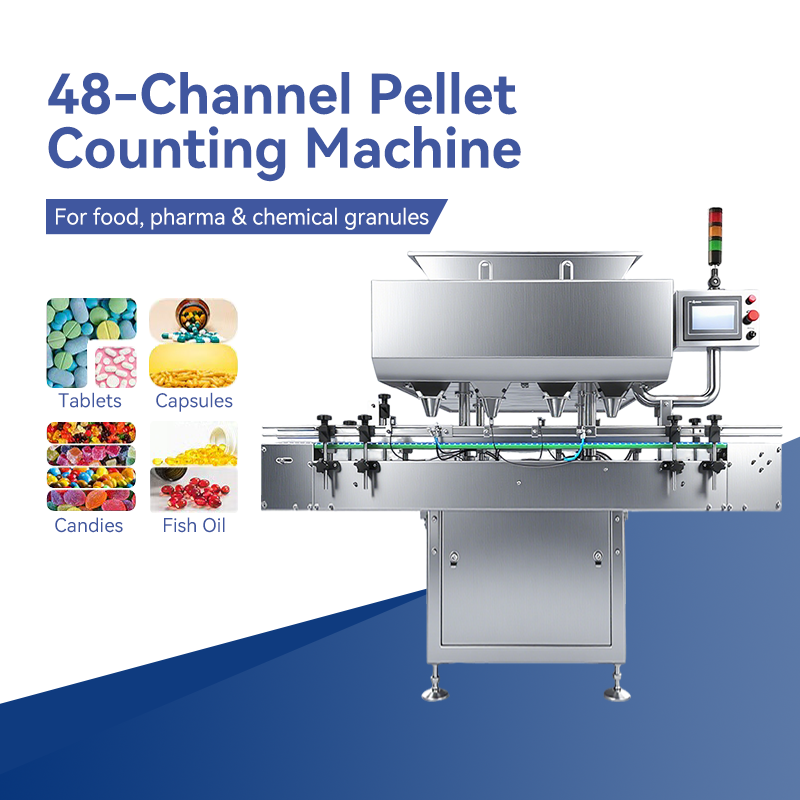
In the core pharmaceutical manufacturing and repackaging sectors, tablet counters play an indispensable role, widely used for high-speed, precise counting in the bottling, blister packaging, and filling processes of final products. They also support quality sampling inspections and batch inventory management, making them a crucial tool for ensuring production compliance and minimizing waste. In high-volume pharmacy dispensing scenarios, particularly in retail chains and mail-order pharmacies, automated counting significantly reduces waiting times and minimizes human errors, allowing pharmacists to focus more on patient consultation services. Centralized distribution centers rely on counters to achieve precise and efficient processing of thousands of prescriptions daily.
In compounding pharmacies and clinical research environments, precision is critical. Counters are not only used to ensure the precise quantity of active ingredients in customized medications but also support blind packaging of investigational drugs in clinical trials, ensuring the reliability and integrity of trial data. Additionally, in the rapidly growing nutritional supplement industry, counters help companies maintain brand reputation and meet increasingly stringent GMP regulations. Similarly, the veterinary pharmaceutical and animal health sectors leverage this technology to safely and efficiently handle medications of various sizes for both domestic pets and livestock.
In the future, with the development of Industry 4.0 and the Internet of Things (IoT), tablet counters will be further integrated into smart factory systems, enabling real-time synchronization with inventory management (IMS) and enterprise resource planning (ERP) software to achieve data synchronization and process optimization. IoT-enabled devices can also perform self-monitoring, implement predictive maintenance, and enhance overall production efficiency through data analysis.

20
May
20
May
20
May
20
May
“In the past, manually counting goods was slow and prone to errors, but now it can be done in a few minutes with extremely high accuracy.”
“It's very easy to operate and can be learned quickly, saving us a lot of manpower and time costs.”