EN


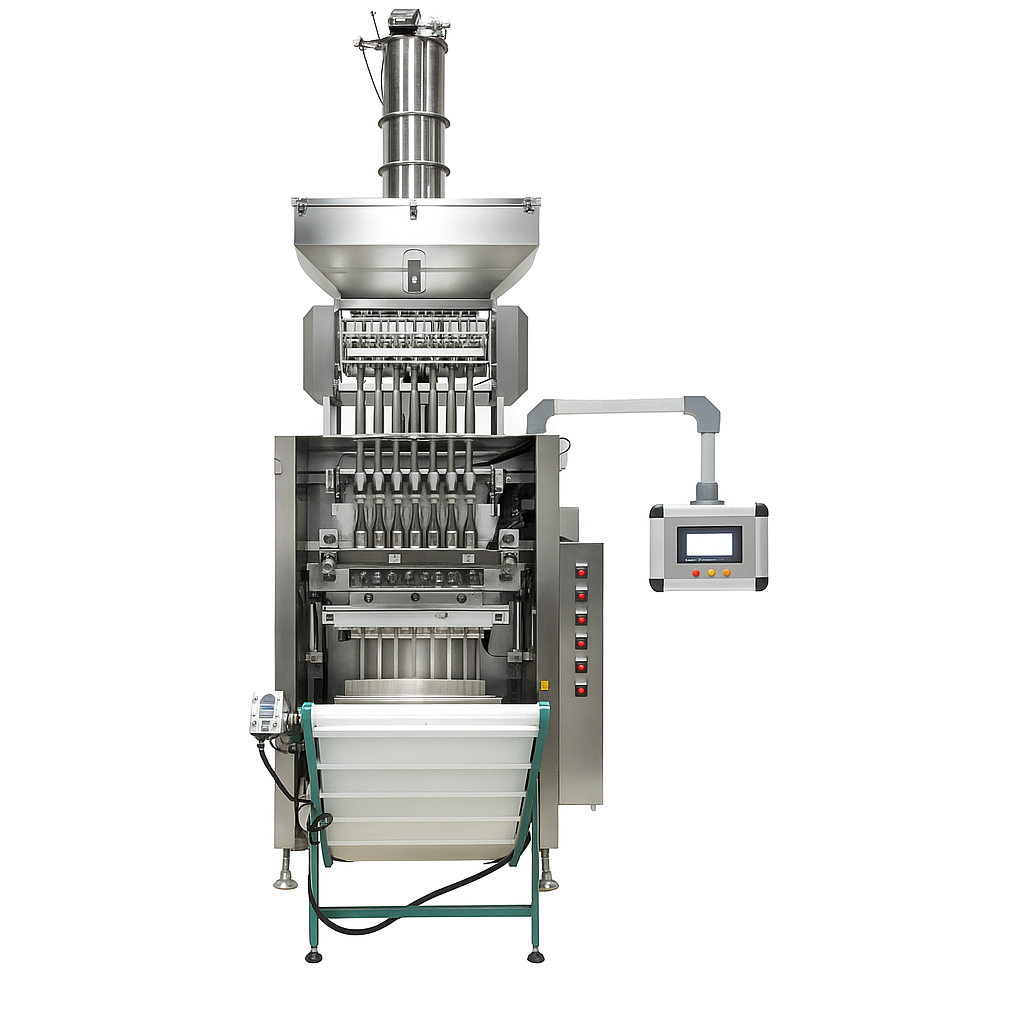
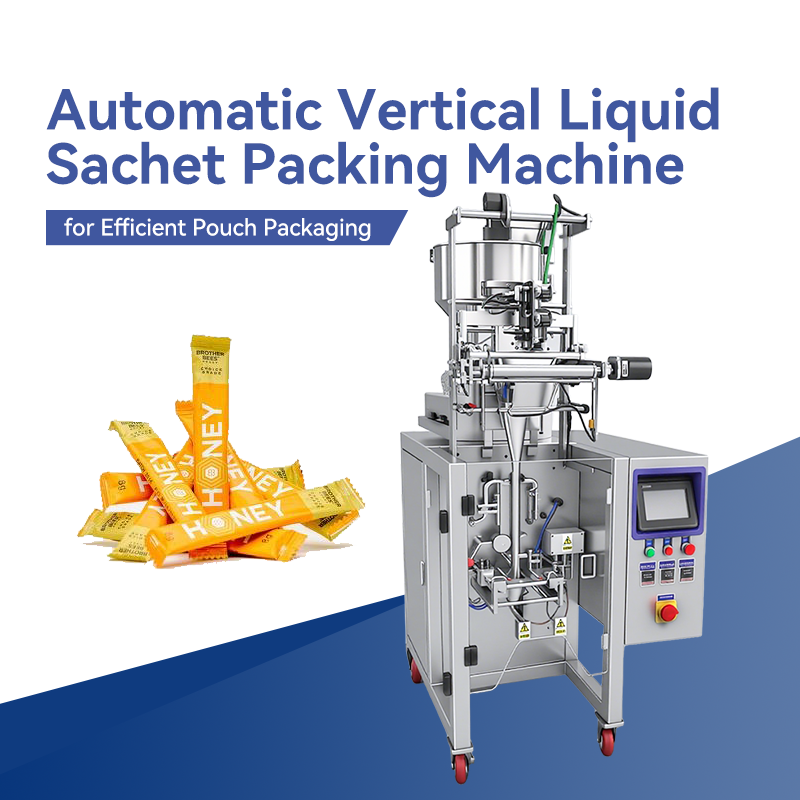
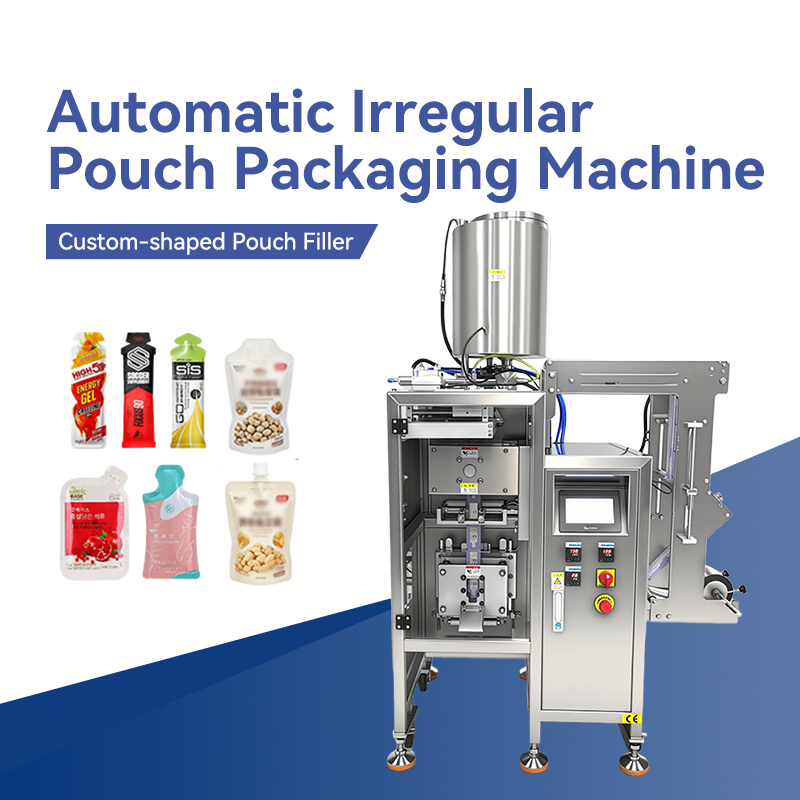
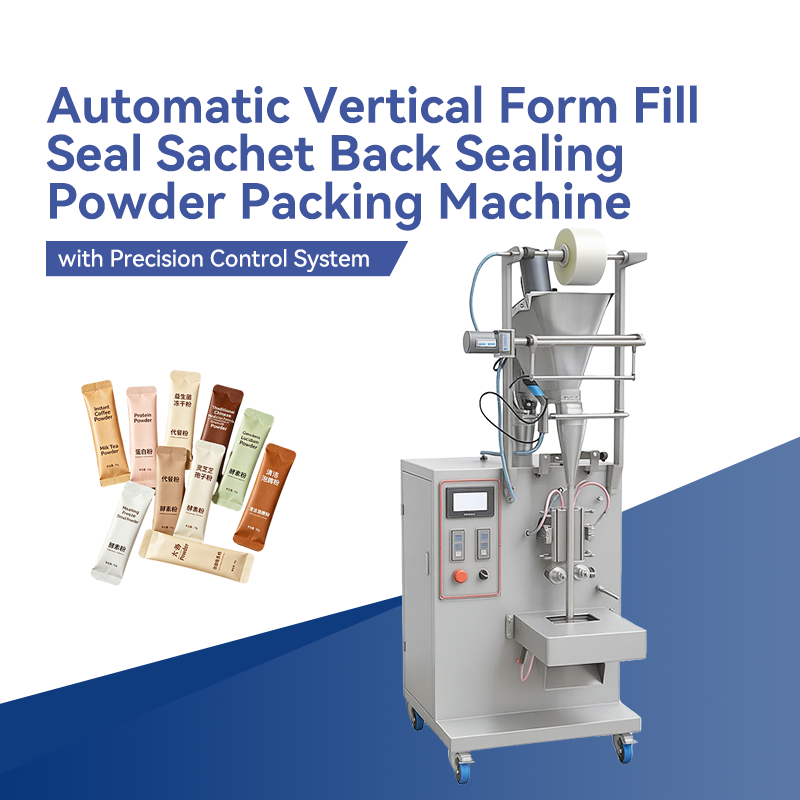
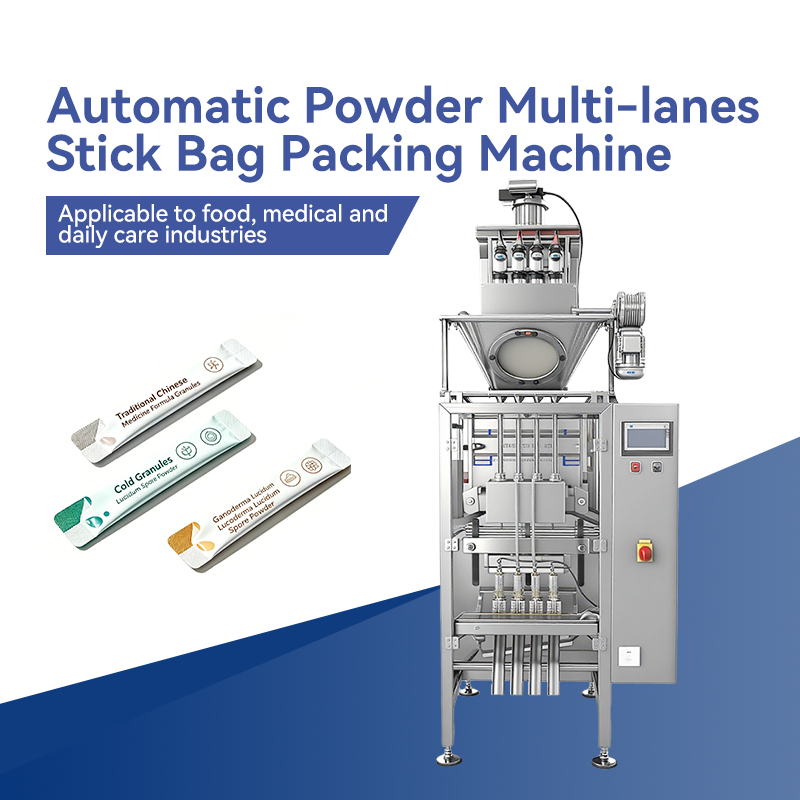
In the field of automated packaging, the importance of packaging machine pouches extends far beyond that of a simple container. They are a core element in ensuring product quality, improving production efficiency, conveying brand value, and achieving sustainability goals. Their primary role is to safeguard product integrity and freshness. High-quality pouches, made using multi-layer composite film technology, effectively block moisture, oxygen, light, and contaminants, significantly extending the shelf life of food, pharmaceuticals, and sensitive chemicals, while ensuring product safety during transportation.
More importantly, there is an efficient synergy between the pouch and the equipment, making it a key factor in the smooth operation of the production line. A well-designed pouch can greatly enhance operational efficiency—its consistent dimensions and reliable sealing layer minimize equipment jams and failures, ensuring a high-speed, high-efficiency production rhythm, thereby directly reducing unit costs and improving profitability.
Additionally, packaging bags serve as silent ambassadors for your brand. They are the first physical point of contact between consumers and products, and their design, print quality, and tactile feel directly influence consumer purchasing decisions and brand perception. A sturdy, aesthetically pleasing bag with convenient features such as easy-tear openings or reusable seals not only enhances shelf appeal but also builds strong brand loyalty through superior user experience.
Finally, modern packaging machine bags are also an important platform for innovation and environmental sustainability. From functional accessories to eco-friendly solutions made from recyclable single materials or compostable materials, choosing advanced bag packaging is a crucial strategic step for businesses to fulfill their sustainability commitments, comply with environmental regulations, and gain the approval of modern consumers.

20
May
20
May
20
May
20
May
"Game-changer for our small biz. Went from hand-filling to professional packs in hours. Paid for itself quickly."
"Runs non-stop on our production line. Incredibly reliable and accurate. Drastically cut our product waste."