EN


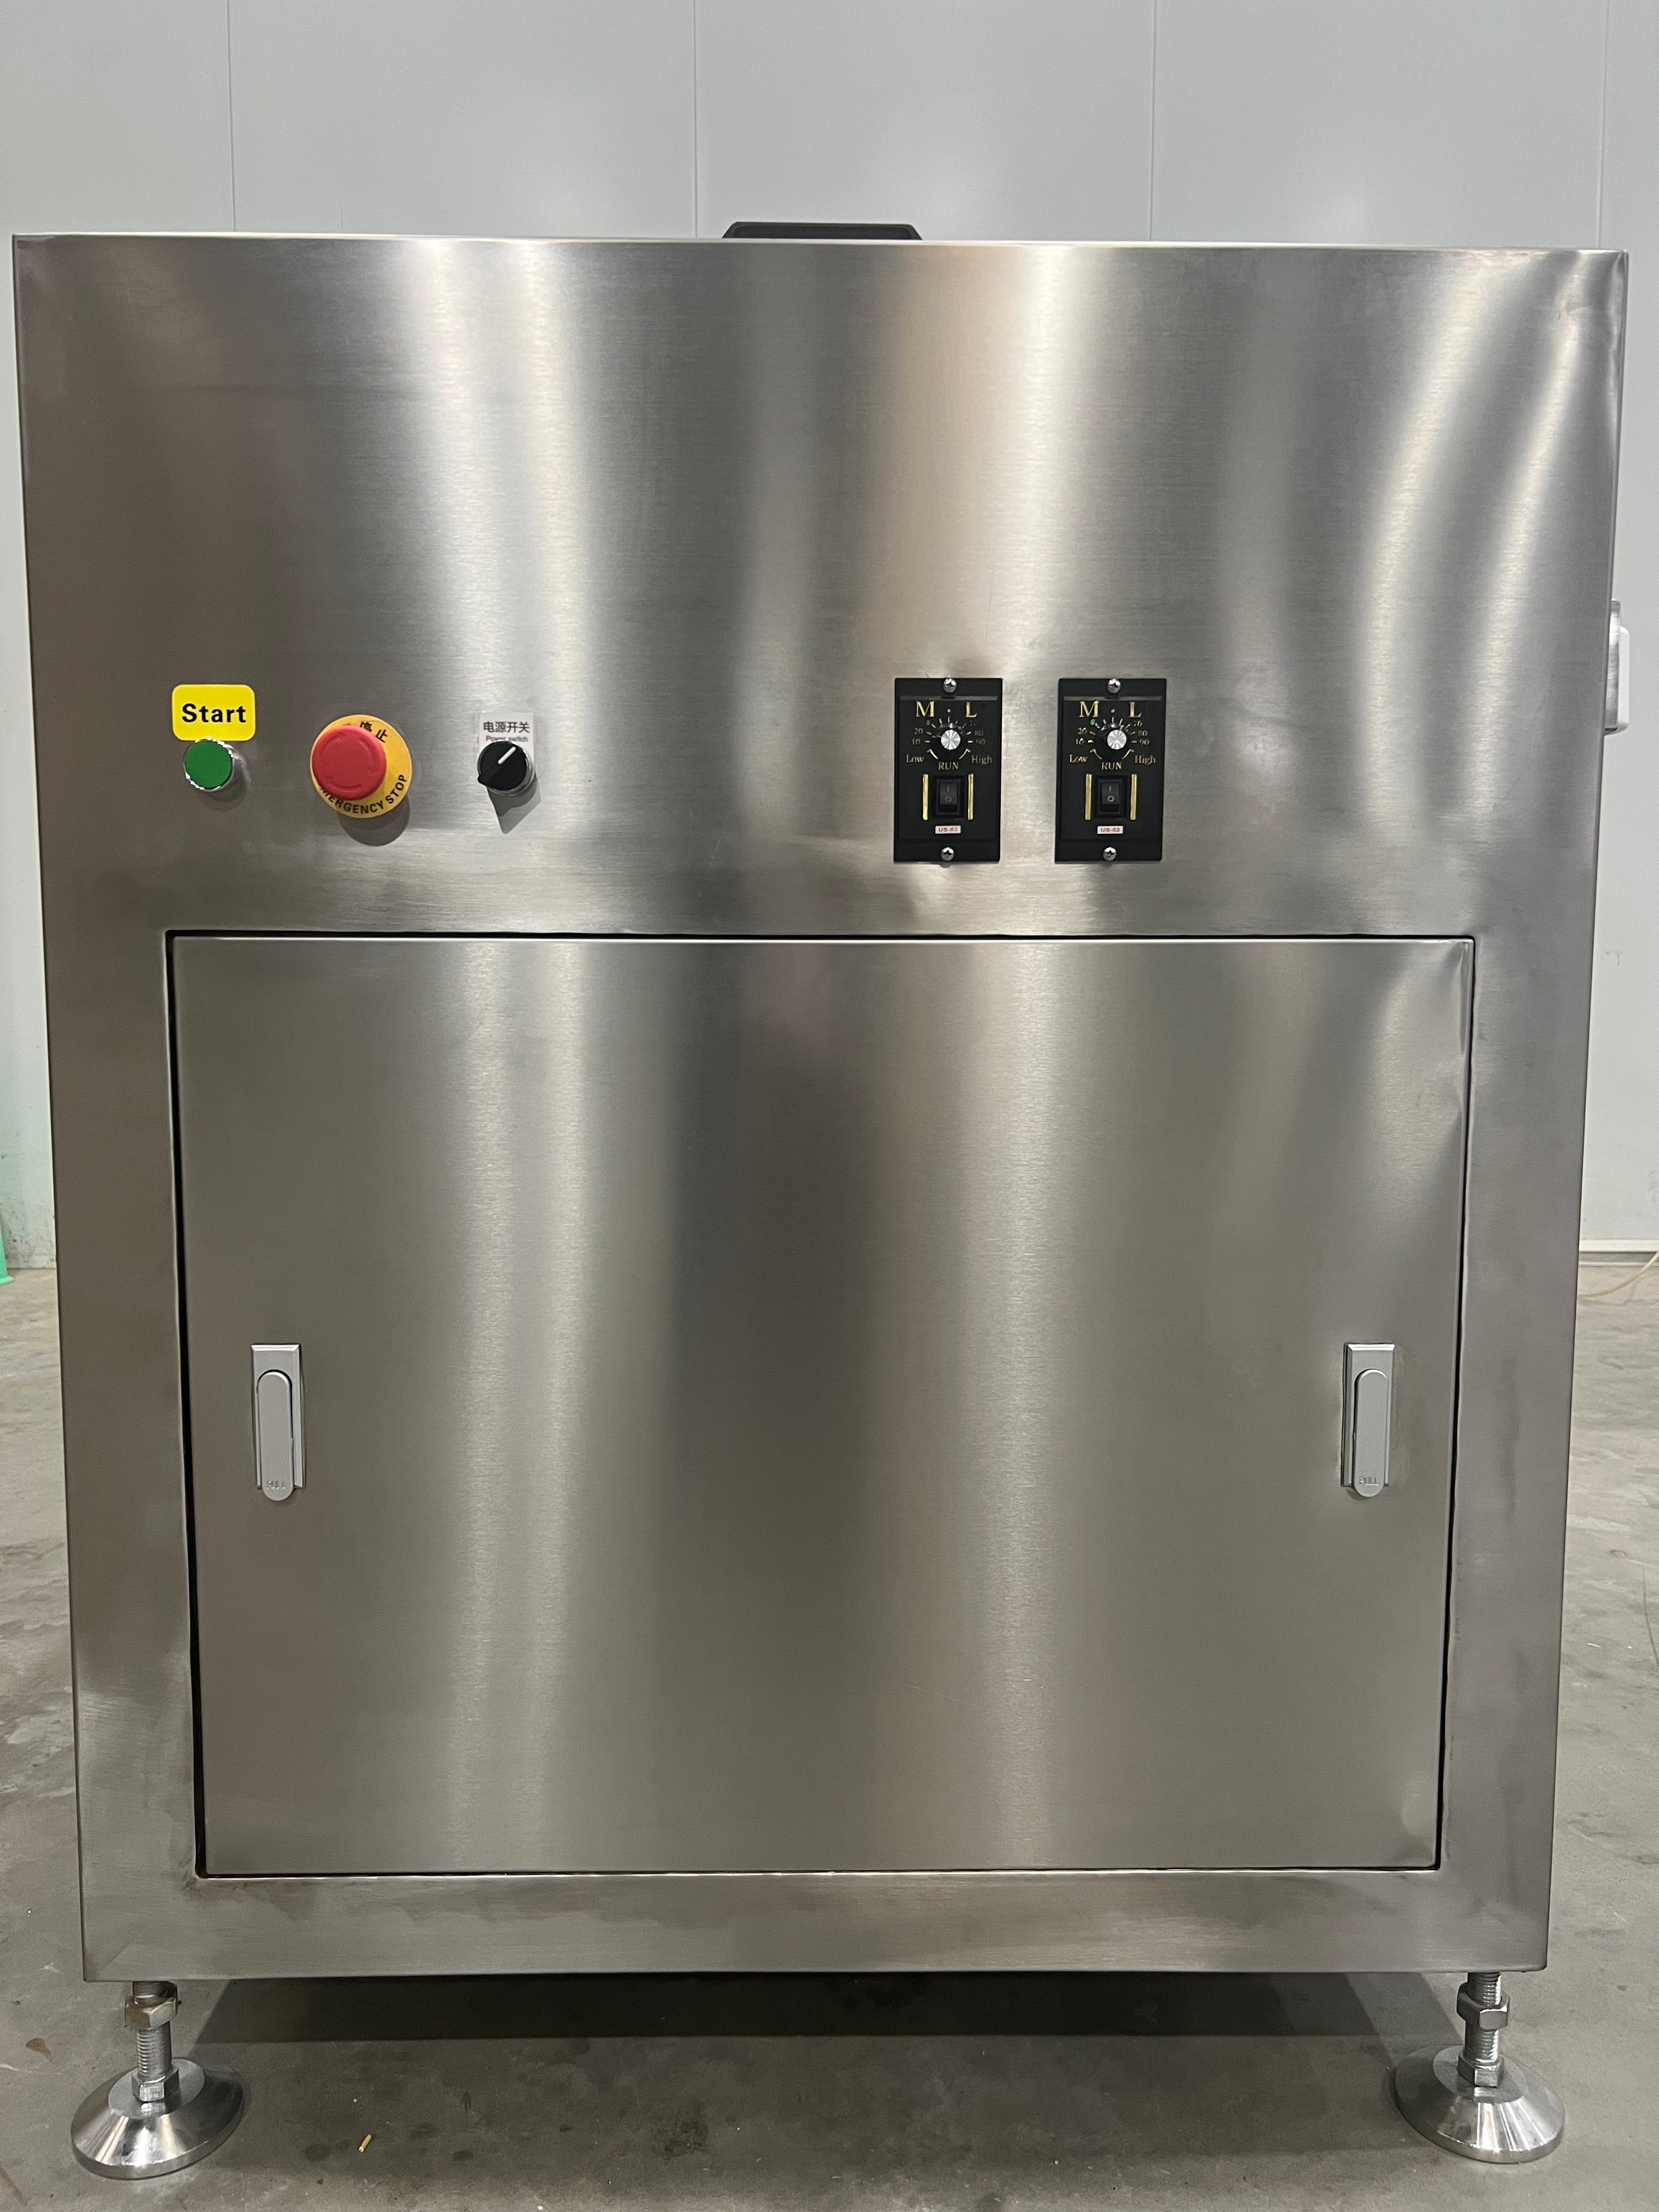
As a core automated device in modern packaging production lines, the automatic high-speed bottle sorting machine has an extremely broad application outlook and has deeply penetrated multiple key industries such as beverages, food, pharmaceuticals, cosmetics, and chemicals. In the beverage sector, this equipment serves as the cornerstone for high-speed production, capable of processing thousands of bottles per minute at ultra-high speeds, seamlessly integrating with filling machines, capping machines, and labeling machines. It completely eliminates the efficiency bottlenecks and production capacity limitations caused by traditional manual feeding, while effortlessly handling the rapid switching of production requirements for multiple product varieties and bottle specifications.
In the food and edible oil market, the bottle sorting machine, with its precise and gentle handling characteristics, can efficiently adapt to various irregularly shaped bottles and materials (such as glass and PET), ensuring that containers are intact and accurately positioned before filling, eliminating leakage risks, and perfectly meeting the dual requirements of hygiene and efficiency for sauces, syrups, yogurt, and dairy products. For highly regulated industries like pharmaceuticals and health supplements, the equipment's fully automatic, zero-contact operation mode significantly reduces the risk of human contamination, providing sterile, traceable processing solutions compliant with GMP standards for pharmaceutical bottles and nutritional supplement packaging.
The cosmetics and personal care industry also benefits from this technology. High-end perfume bottles and skincare containers often feature unique designs and delicate materials. The machine's gentle handling mechanism effectively prevents scratches and impacts, maintaining the product's flawless appearance even at high speeds, providing a robust production foundation for brand-innovative packaging designs. In the chemical and household goods sectors, the equipment's robust durability and material compatibility enable stable processing of large chemical containers and detergent bottles, demonstrating the technology's broad adaptability.
Looking ahead, the application prospects of automatic high-speed bottle sorting machines are closely integrated with Industry 4.0 and smart manufacturing. By integrating IoT sensors, the equipment can achieve real-time performance monitoring, predictive maintenance, and data-driven efficiency management (OEE); As a key hub in automated production lines, it can efficiently interface with downstream robots to complete palletizing, packaging, and other processes, and supports high-speed processing of lightweight and recyclable materials (such as rPET) bottles, helping enterprises achieve green manufacturing goals. In summary, the automatic high-speed bottle sorting machine is not only a core tool for enhancing production capacity and flexibility but also a strategic asset for enterprises embracing digital and intelligent production transformation.

20
May
20
May
20
May
20
May
"We were constantly dealing with bottlenecks and jams at the start of our line. Since installing this machine, the flow is seamless. It just works, shift after shift. The reliability is incredible and it's completely eliminated the manual sorting we used to have to do."
"We run multiple SKUs with different bottle sizes, so changeover time is critical. The tool-less adjustment on this model is the real deal. What used to take us an hour now takes minutes. Our downtime has plummeted, and our team finds it very intuitive to operate."