EN


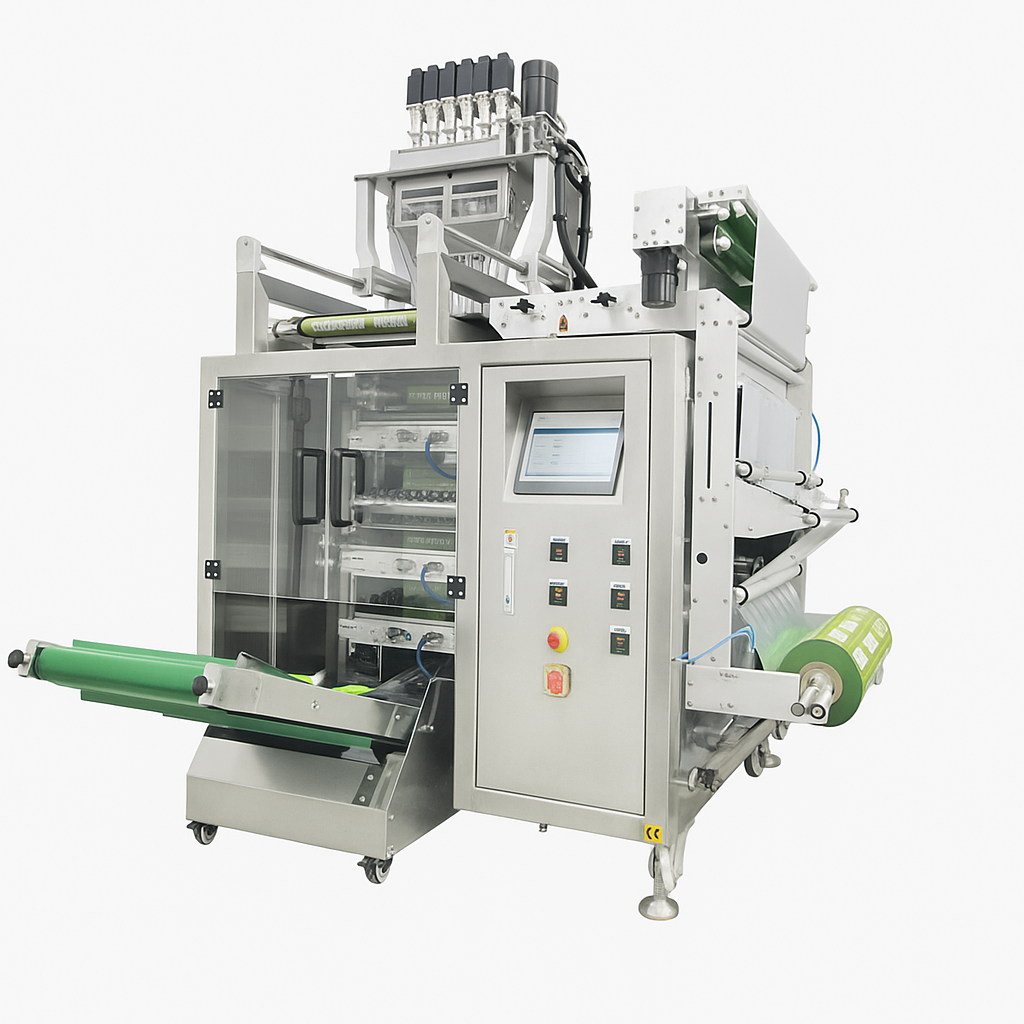
The application areas of pill blister pack machines are extremely broad, far beyond traditional pharmaceutical packaging. Their core value lies in providing efficient, precise, and product-integrity-ensuring packaging solutions, making them the preferred technology across numerous industries. In the pharmaceutical sector, they are the global standard for unit-dose packaging, offering precise dose control, superior moisture and light protection, and effectively enhancing patient medication adherence for both prescription and over-the-counter drugs. Similarly, in the nutritional supplements and vitamin industry, the machine produces professional-looking, tamper-resistant packaging that perfectly protects sensitive ingredients such as probiotics and soft gel capsules, while supporting customized daily nutritional combination packaging. In the veterinary pharmaceutical sector, it ensures accurate drug dosing for pets and livestock in complex environments. Additionally, its principles are highly applicable to the consumer electronics and food industries, creating aesthetically pleasing, safe, tamper-proof, and durable “blister” retail packaging for products like batteries, small electronic devices, gum, and coffee capsules, fully demonstrating its technical versatility and reliability.

20
May
20
May
20
May
20
May
“Precise and efficient, ideal for small-batch production, with extremely convenient material changeovers.”
“The most reliable equipment on the production line, stable long-term operation, and easy employee training.”