EN


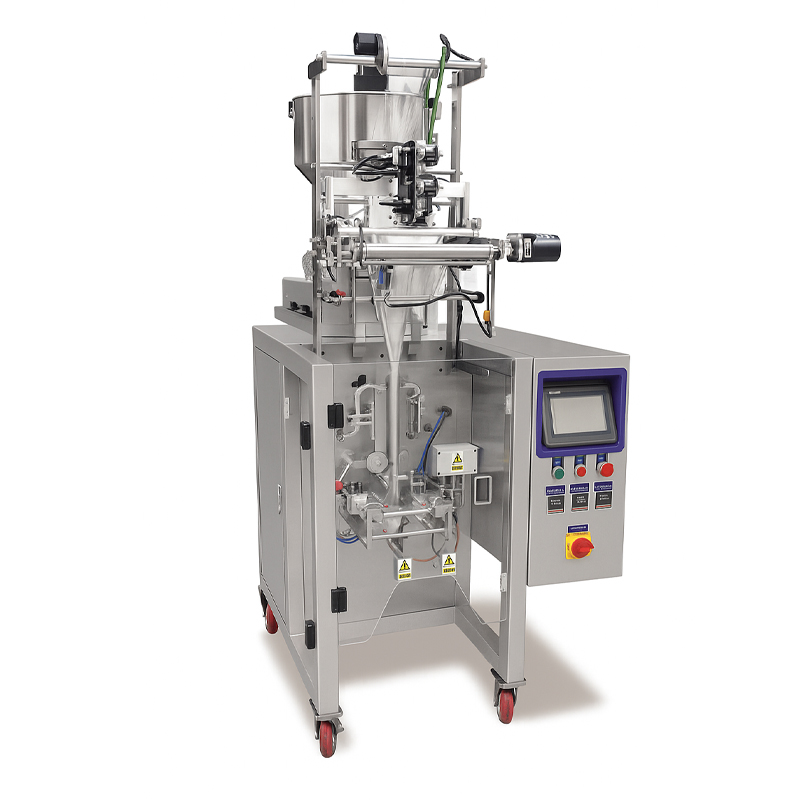
Multifunctional Applications and Core Industry Analysis of Automated Bagging Packaging Machines
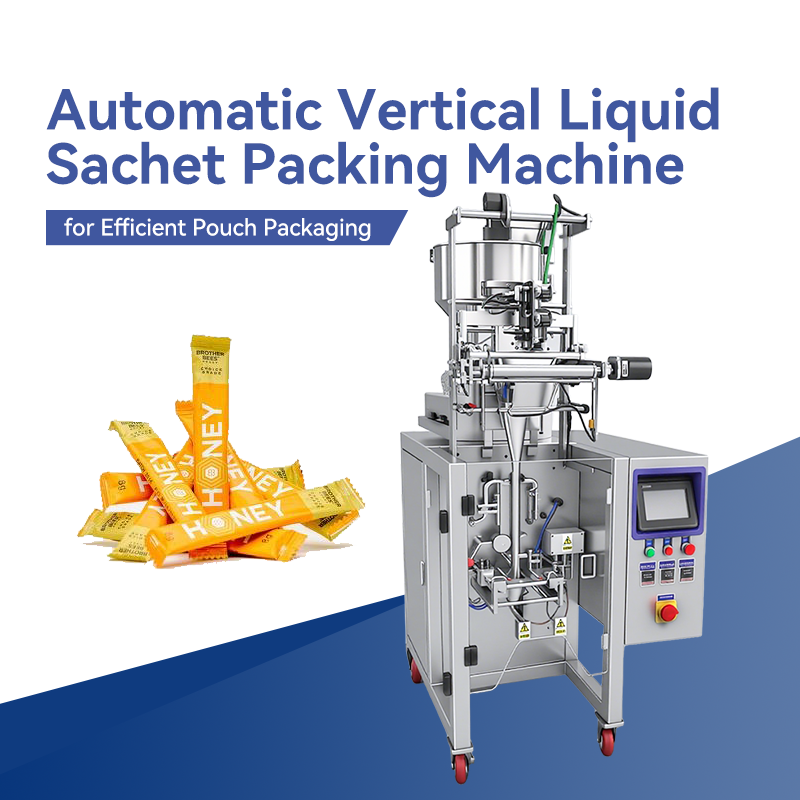
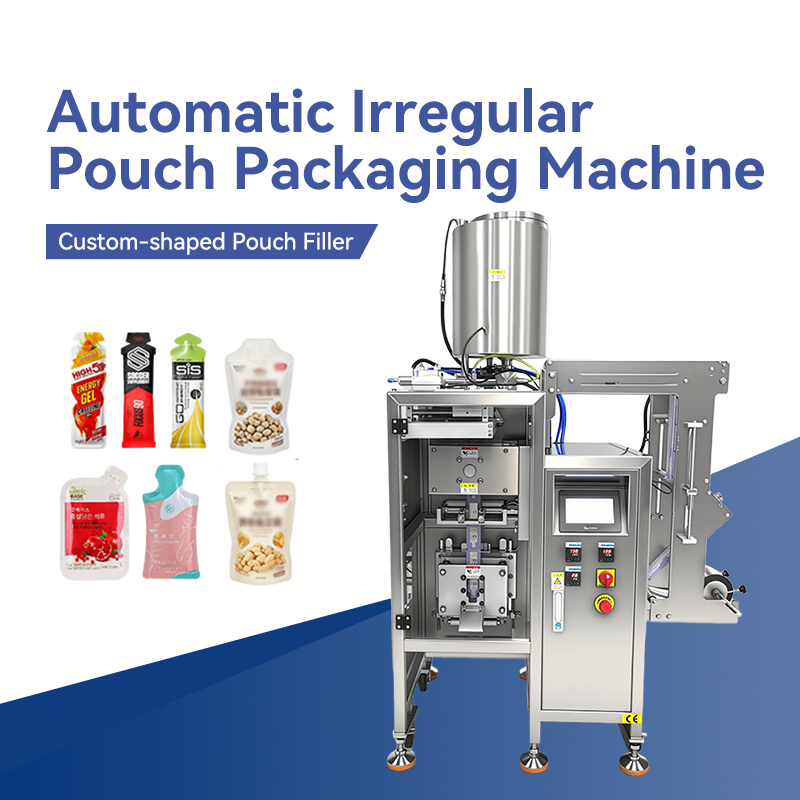
As a critical piece of equipment in modern industrial production, automated bagging packaging machines boast an extensive range of applications spanning multiple core industries. In the food and beverage sector, these machines efficiently process grains, cereals, flour, sugars, snacks, coffee, and pet food. They ensure packaging meets hygiene standards while delivering high-precision weighing capabilities to minimize waste. Constructed from food-grade materials like 304/316 stainless steel, they feature easy-clean designs and integrated metal detection for product safety.
In the chemicals and minerals sector, automated bagging machines demonstrate exceptional durability and safety, handling abrasive materials like fertilizers, industrial chemicals, construction materials (e.g., cement and sand), and mineral ores. These machines are engineered with corrosion resistance, dustproofing, and explosion-proof features to withstand harsh environments and ensure stable production line operation. Agriculture and animal feed sectors similarly rely on such equipment for packaging feed pellets, seeds, and bulk grains. Their high capacity and robust construction support continuous farm operations while accommodating various bag types (e.g., woven polypropylene bags and paper sacks).
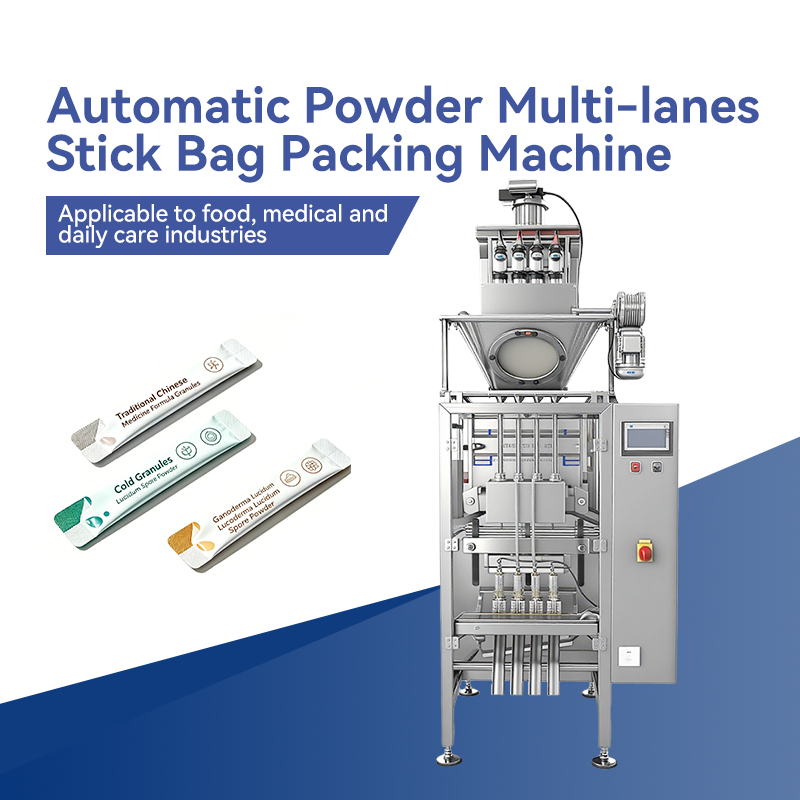
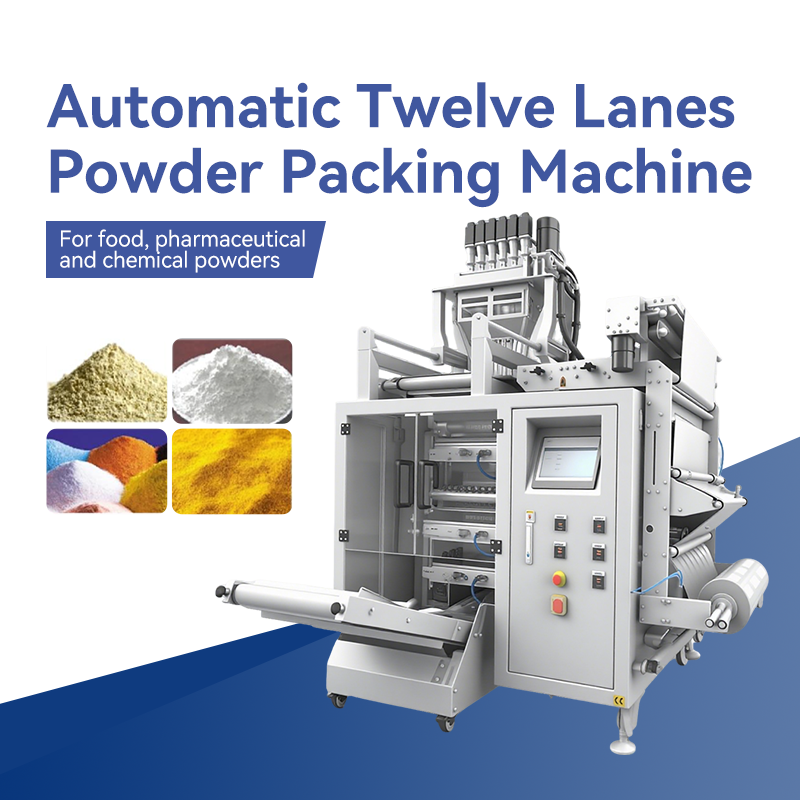
The pharmaceutical and nutritional supplement industries demand extreme precision and compliance in packaging. Automated bagging machines handle powdered supplements, active pharmaceutical ingredients (APIs), and herbal products. Constructed entirely of stainless steel, these machines deliver validated weighing accuracy and comply with cGMP standards, ensuring safe packaging within controlled environments. Furthermore, their versatility extends to landscaping (soil, mulch), recycled plastics (reclaimed flakes), and cosmetics (bath salts, powdered makeup), highlighting their multifunctional capabilities.

20
May
20
May
20
May
20
May
“Precise and efficient, ideal for small-batch production, with extremely convenient material changeovers.”
“The most reliable equipment on the production line, stable long-term operation, and easy employee training.”